Standard configuration
25 equipment items
CLC PHYSICAL-FOAMING LINE
PROCESS ROUTEPhysical foaming · Non-autoclaved curing
CLC / foam concrete block production using physical foaming and non-autoclaved curing. Explore the line visual, production stages, equipment configuration, project examples and installation support.
Get a Production Line Proposal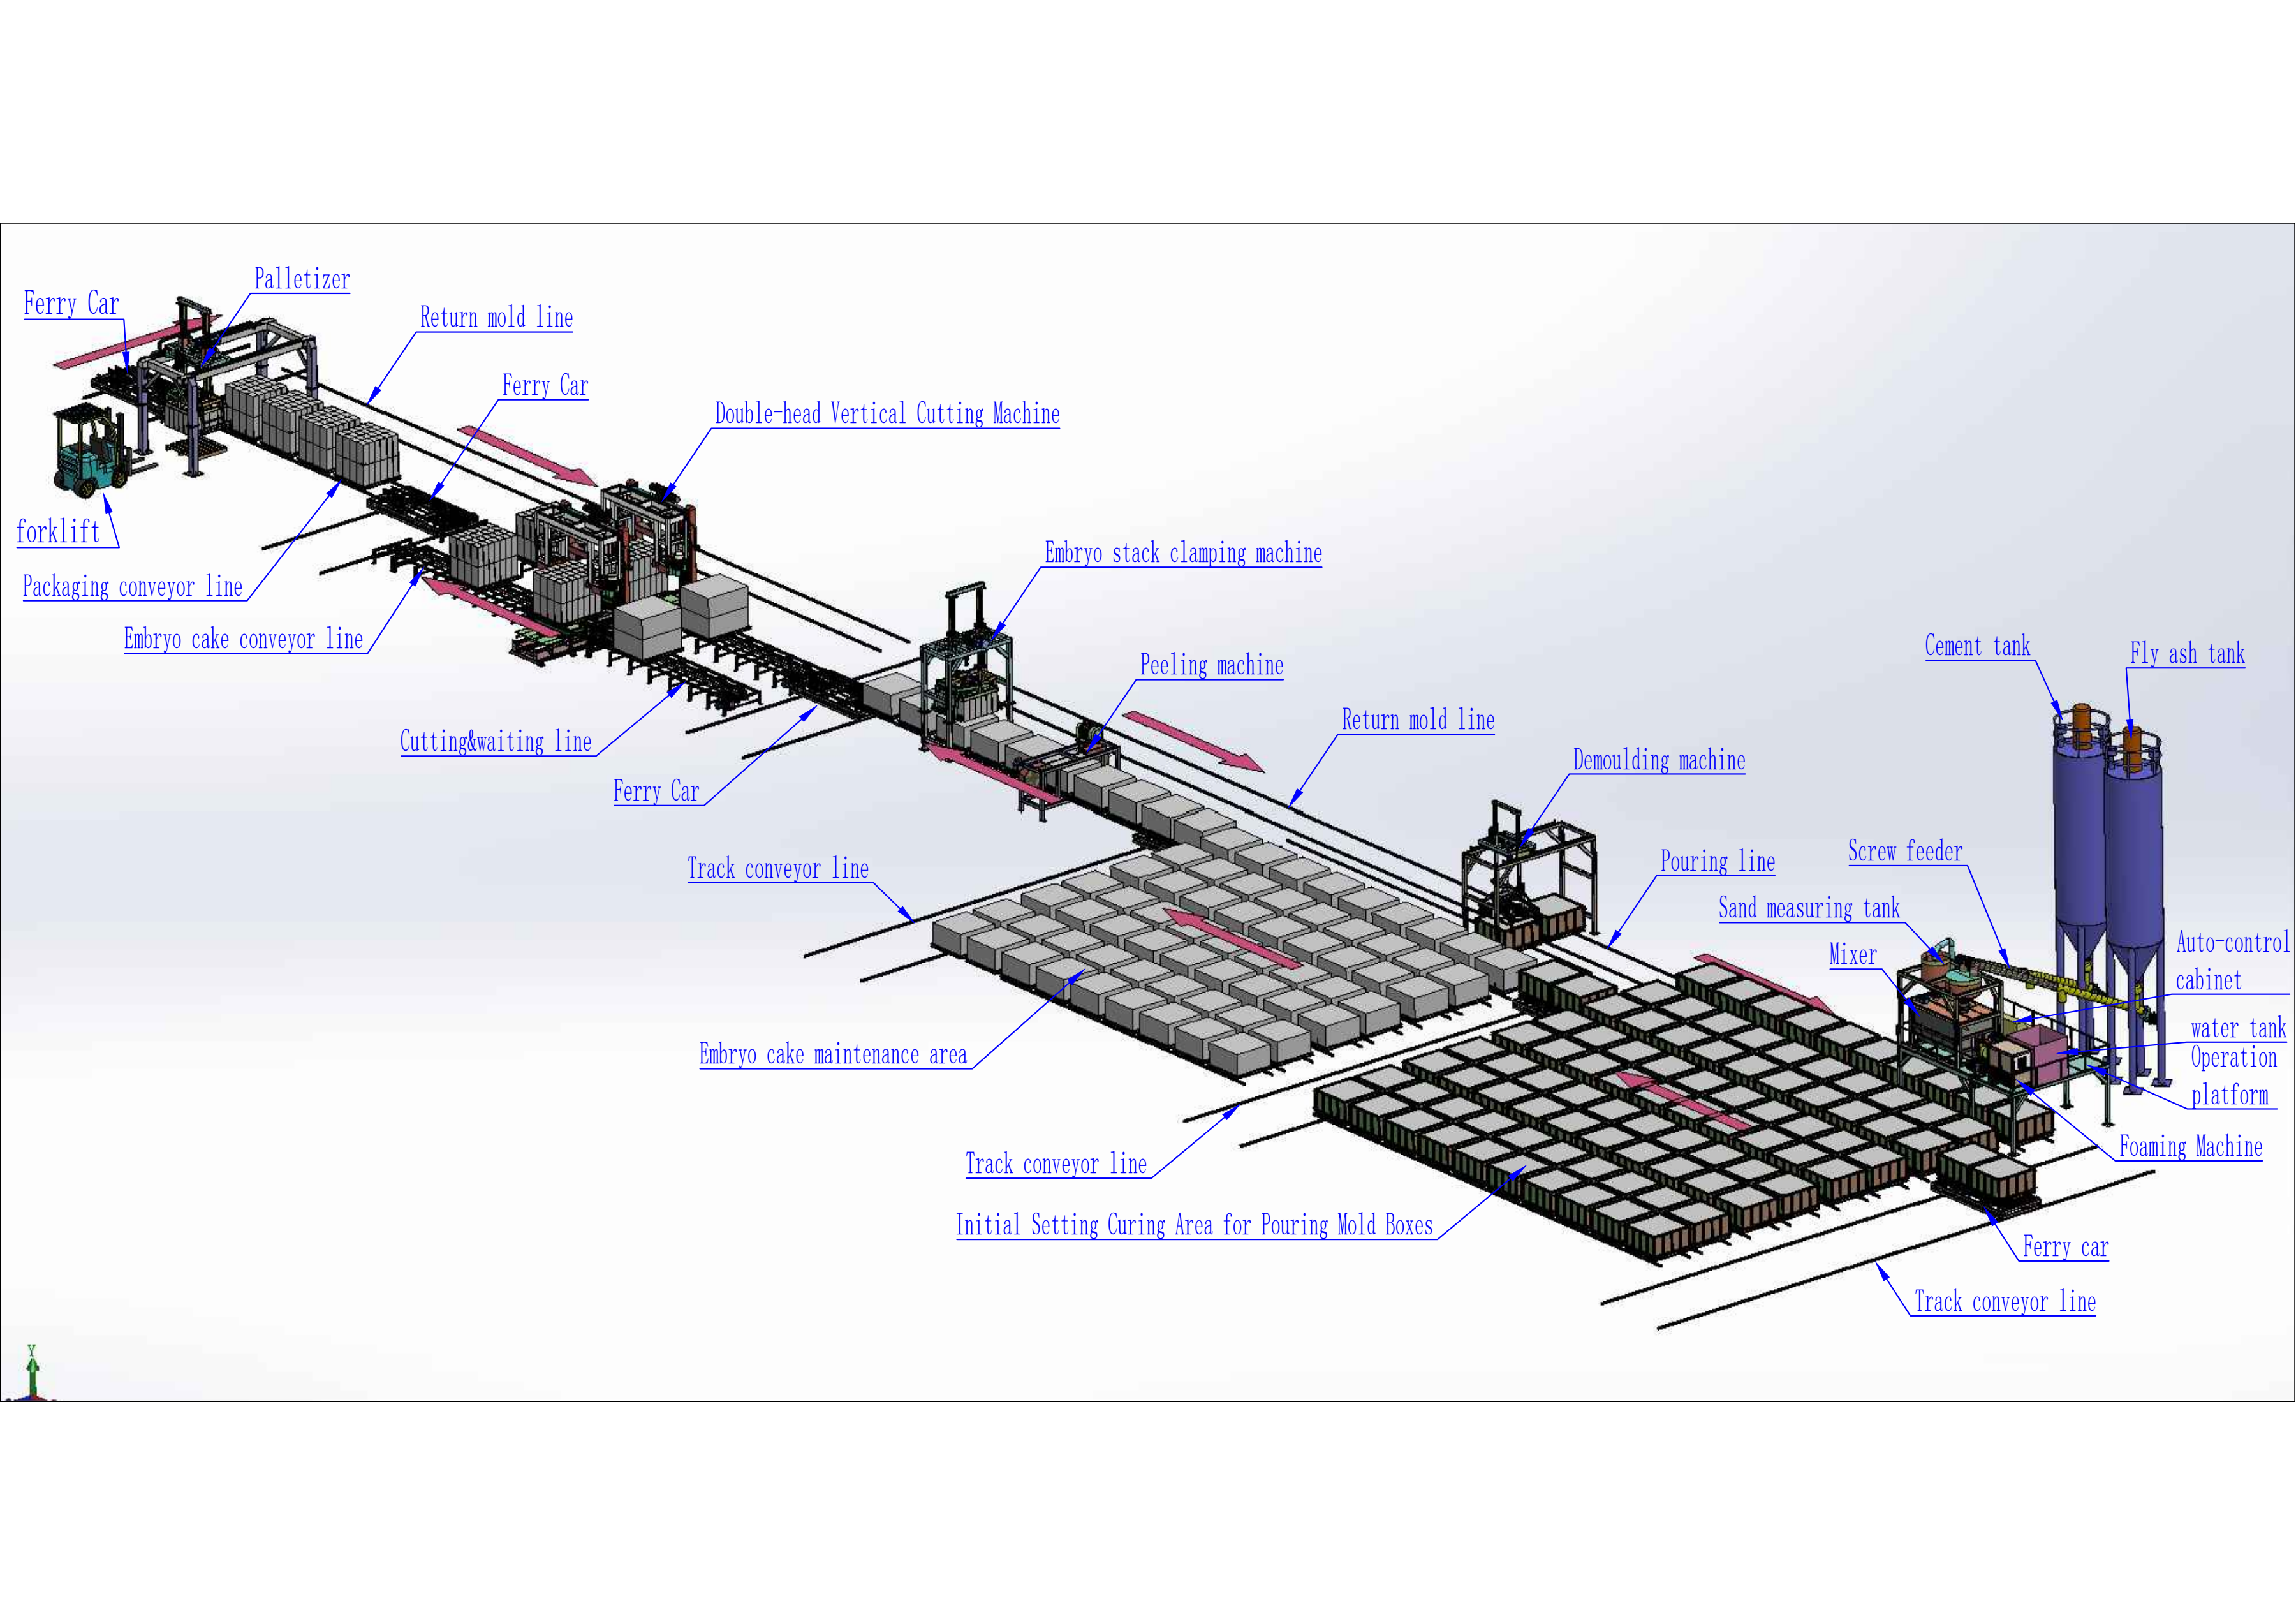 Open full-size layout
CAPACITY QUICK INFORMATION
Based on one 8-hour casting shift. The nominal planning rate of 25 m³/hour is used for engineering calculation and does not represent hourly saleable output. Actual qualified output depends on mould turnover, curing, cutting, handling, reject rate and site conditions.
SOURCE-BACKED CAPACITY DIFFERENCES
AVAILABLE CONFIGURATIONS
Compare equipment configurations for the same planned capacity. The table below shows the primary configuration; our engineers select the applicable route after reviewing your product and raw materials.
25 equipment items
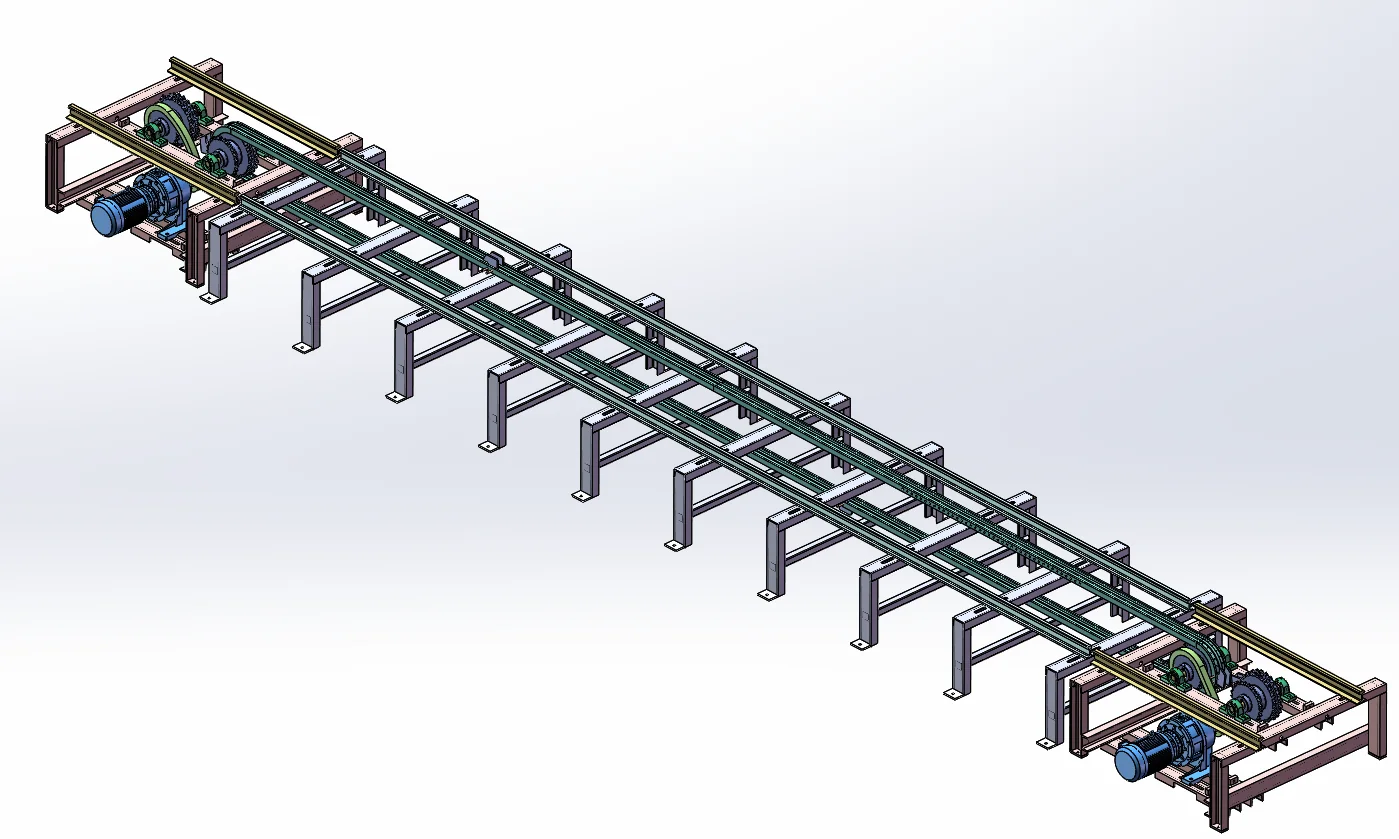
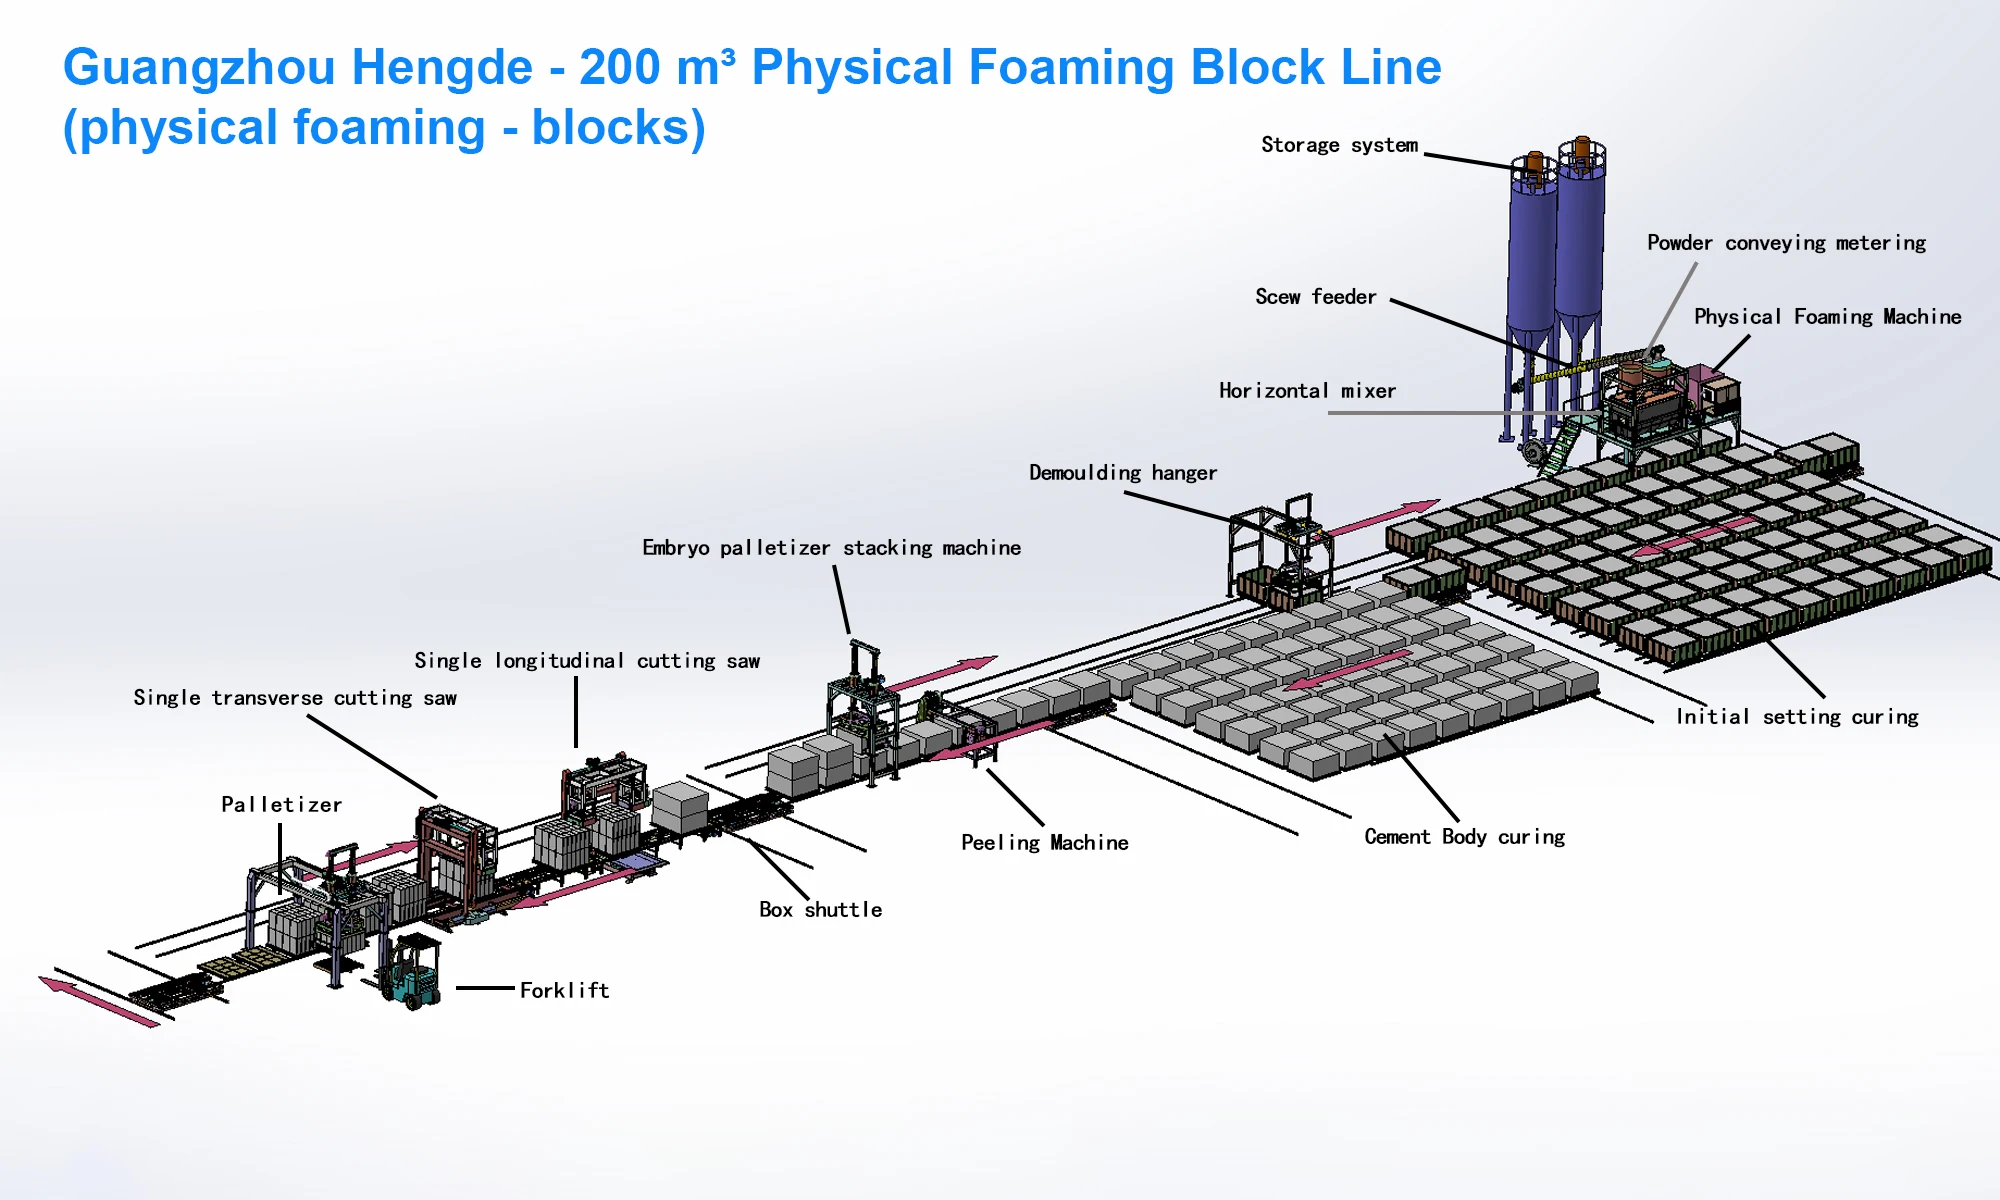 LAYOUT OPTION
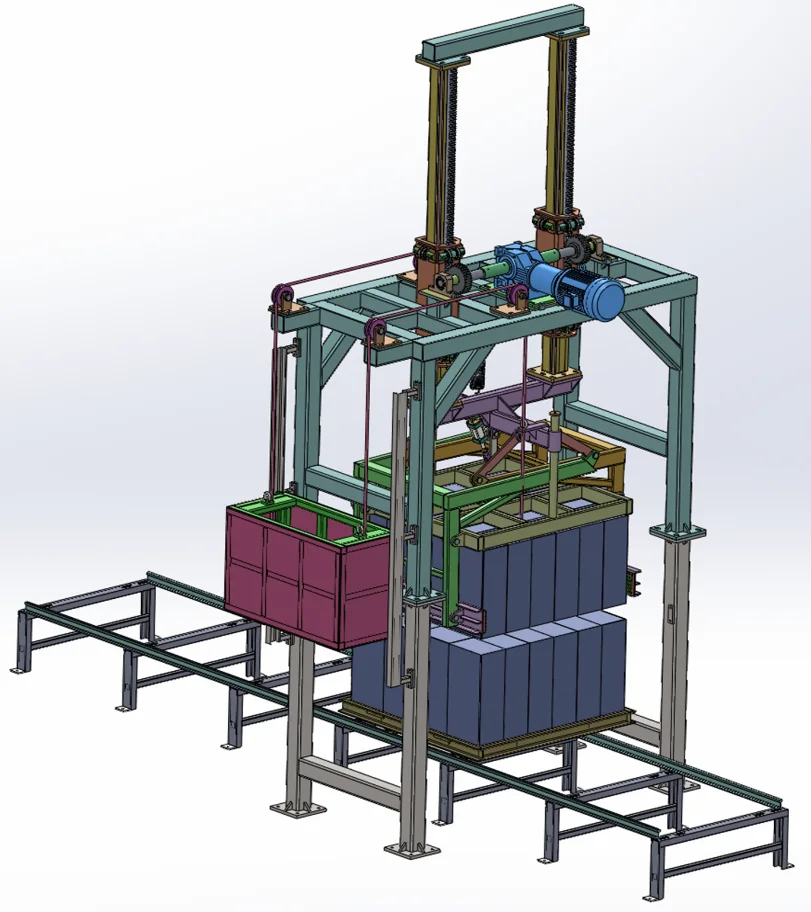
Alternative engineering layout. Its equipment scope is confirmed separately during factory planning and is not included in the standard configuration below.
SIX-STEP PROCESS
Feed and weigh the confirmed powder, aggregate and water inputs.
Prepare preformed physical foam with the source-listed foaming machine and combine it with the metered slurry.
Fill the mould configuration selected for the block product and production capacity.
Match the non-autoclaved curing time, mould count and demoulding condition to the product.
Use only the cutting architecture listed for this capacity and variant.
Move finished blocks through the source-listed handling and stacking scope.
COMPLETE EQUIPMENT CONFIGURATION
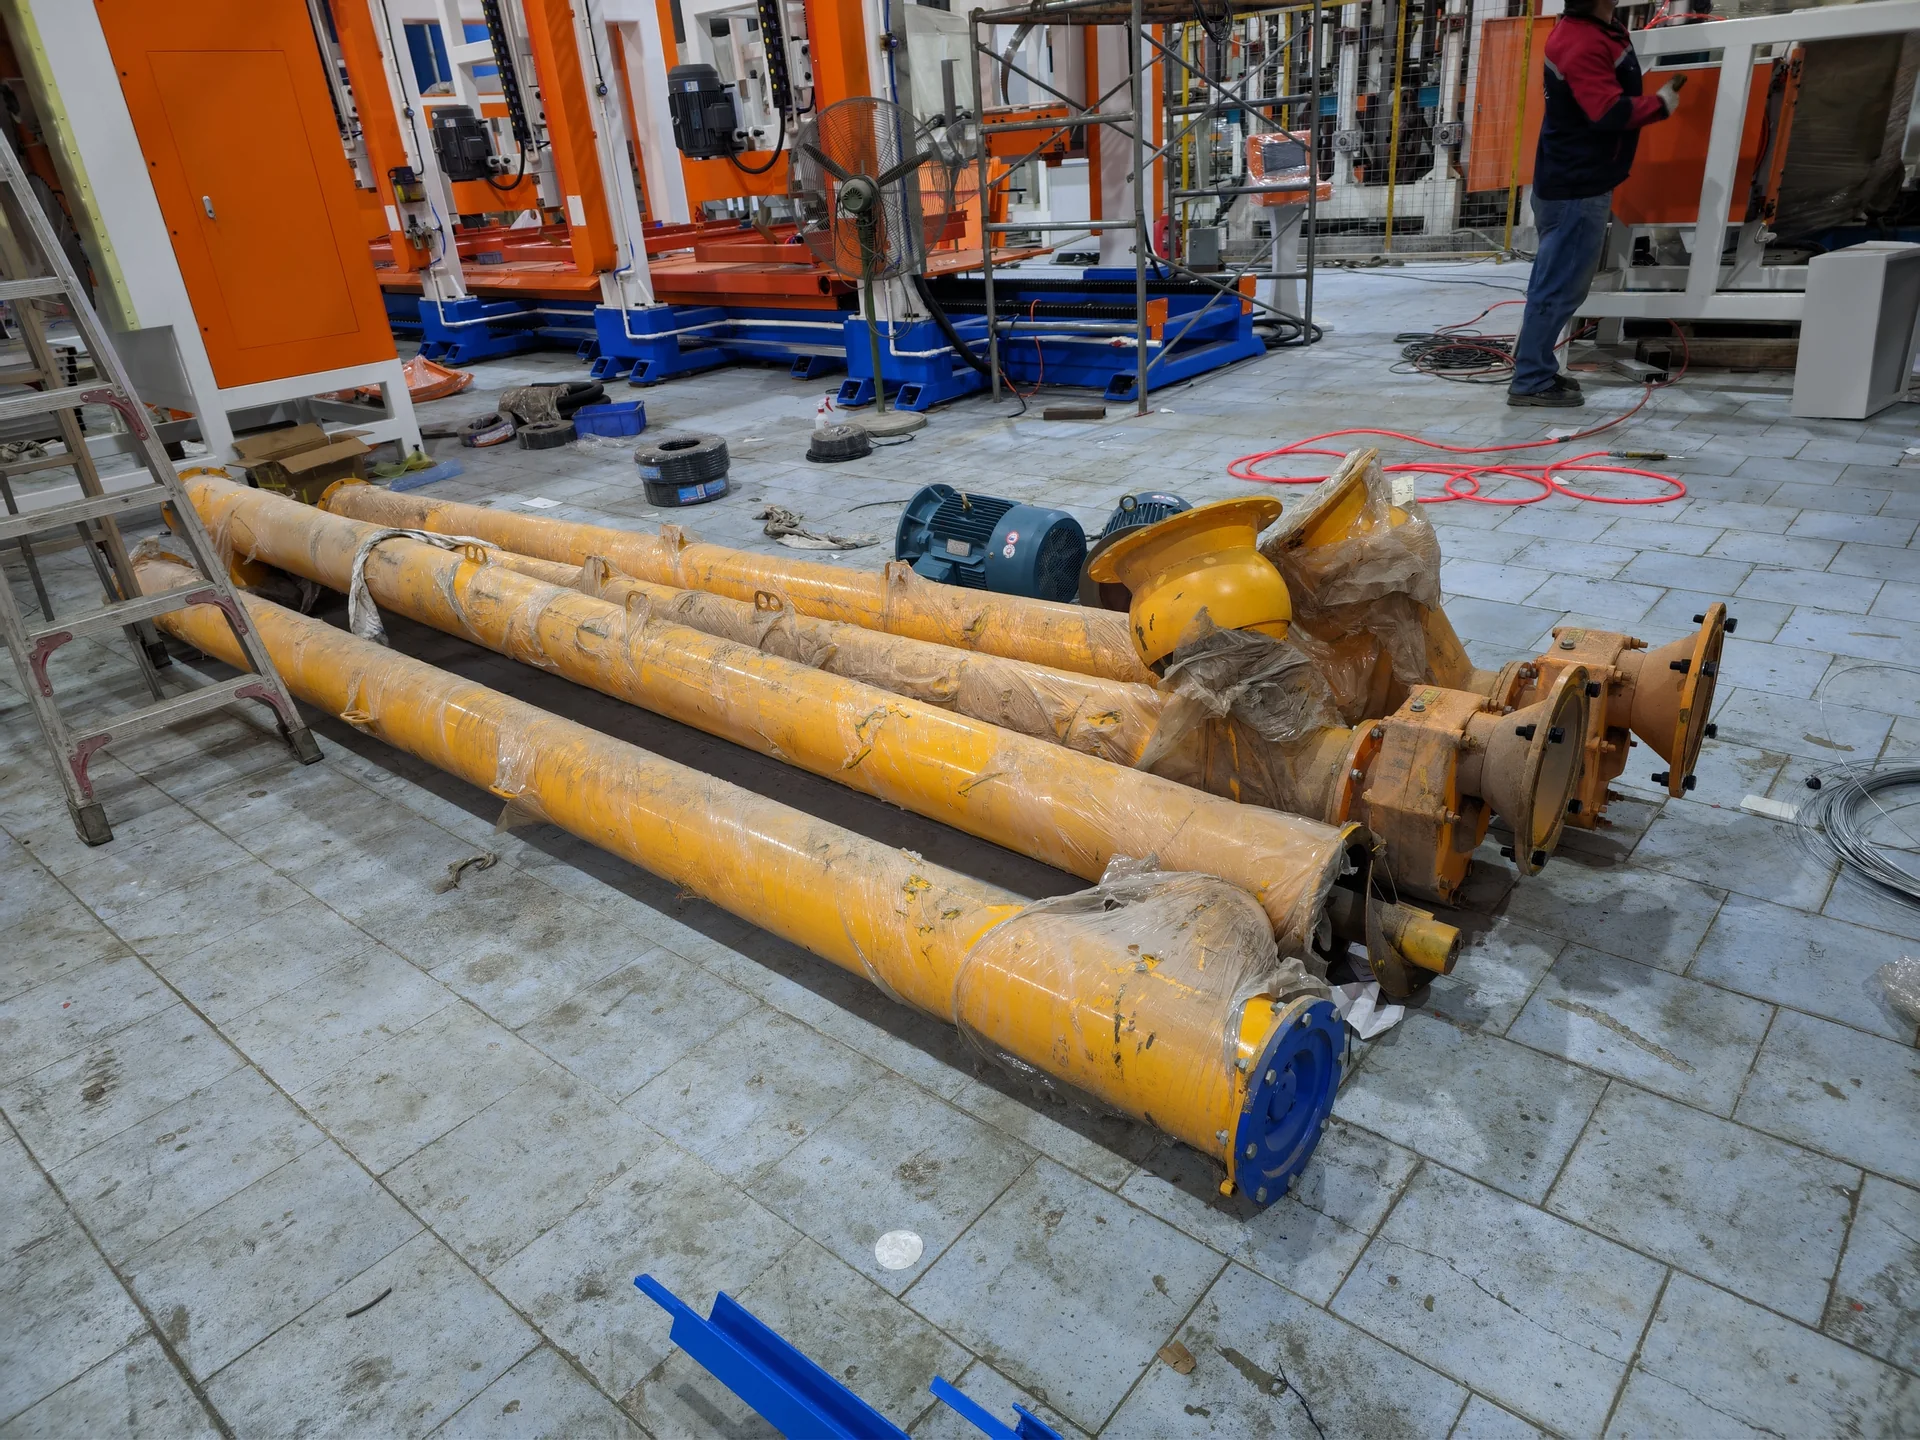
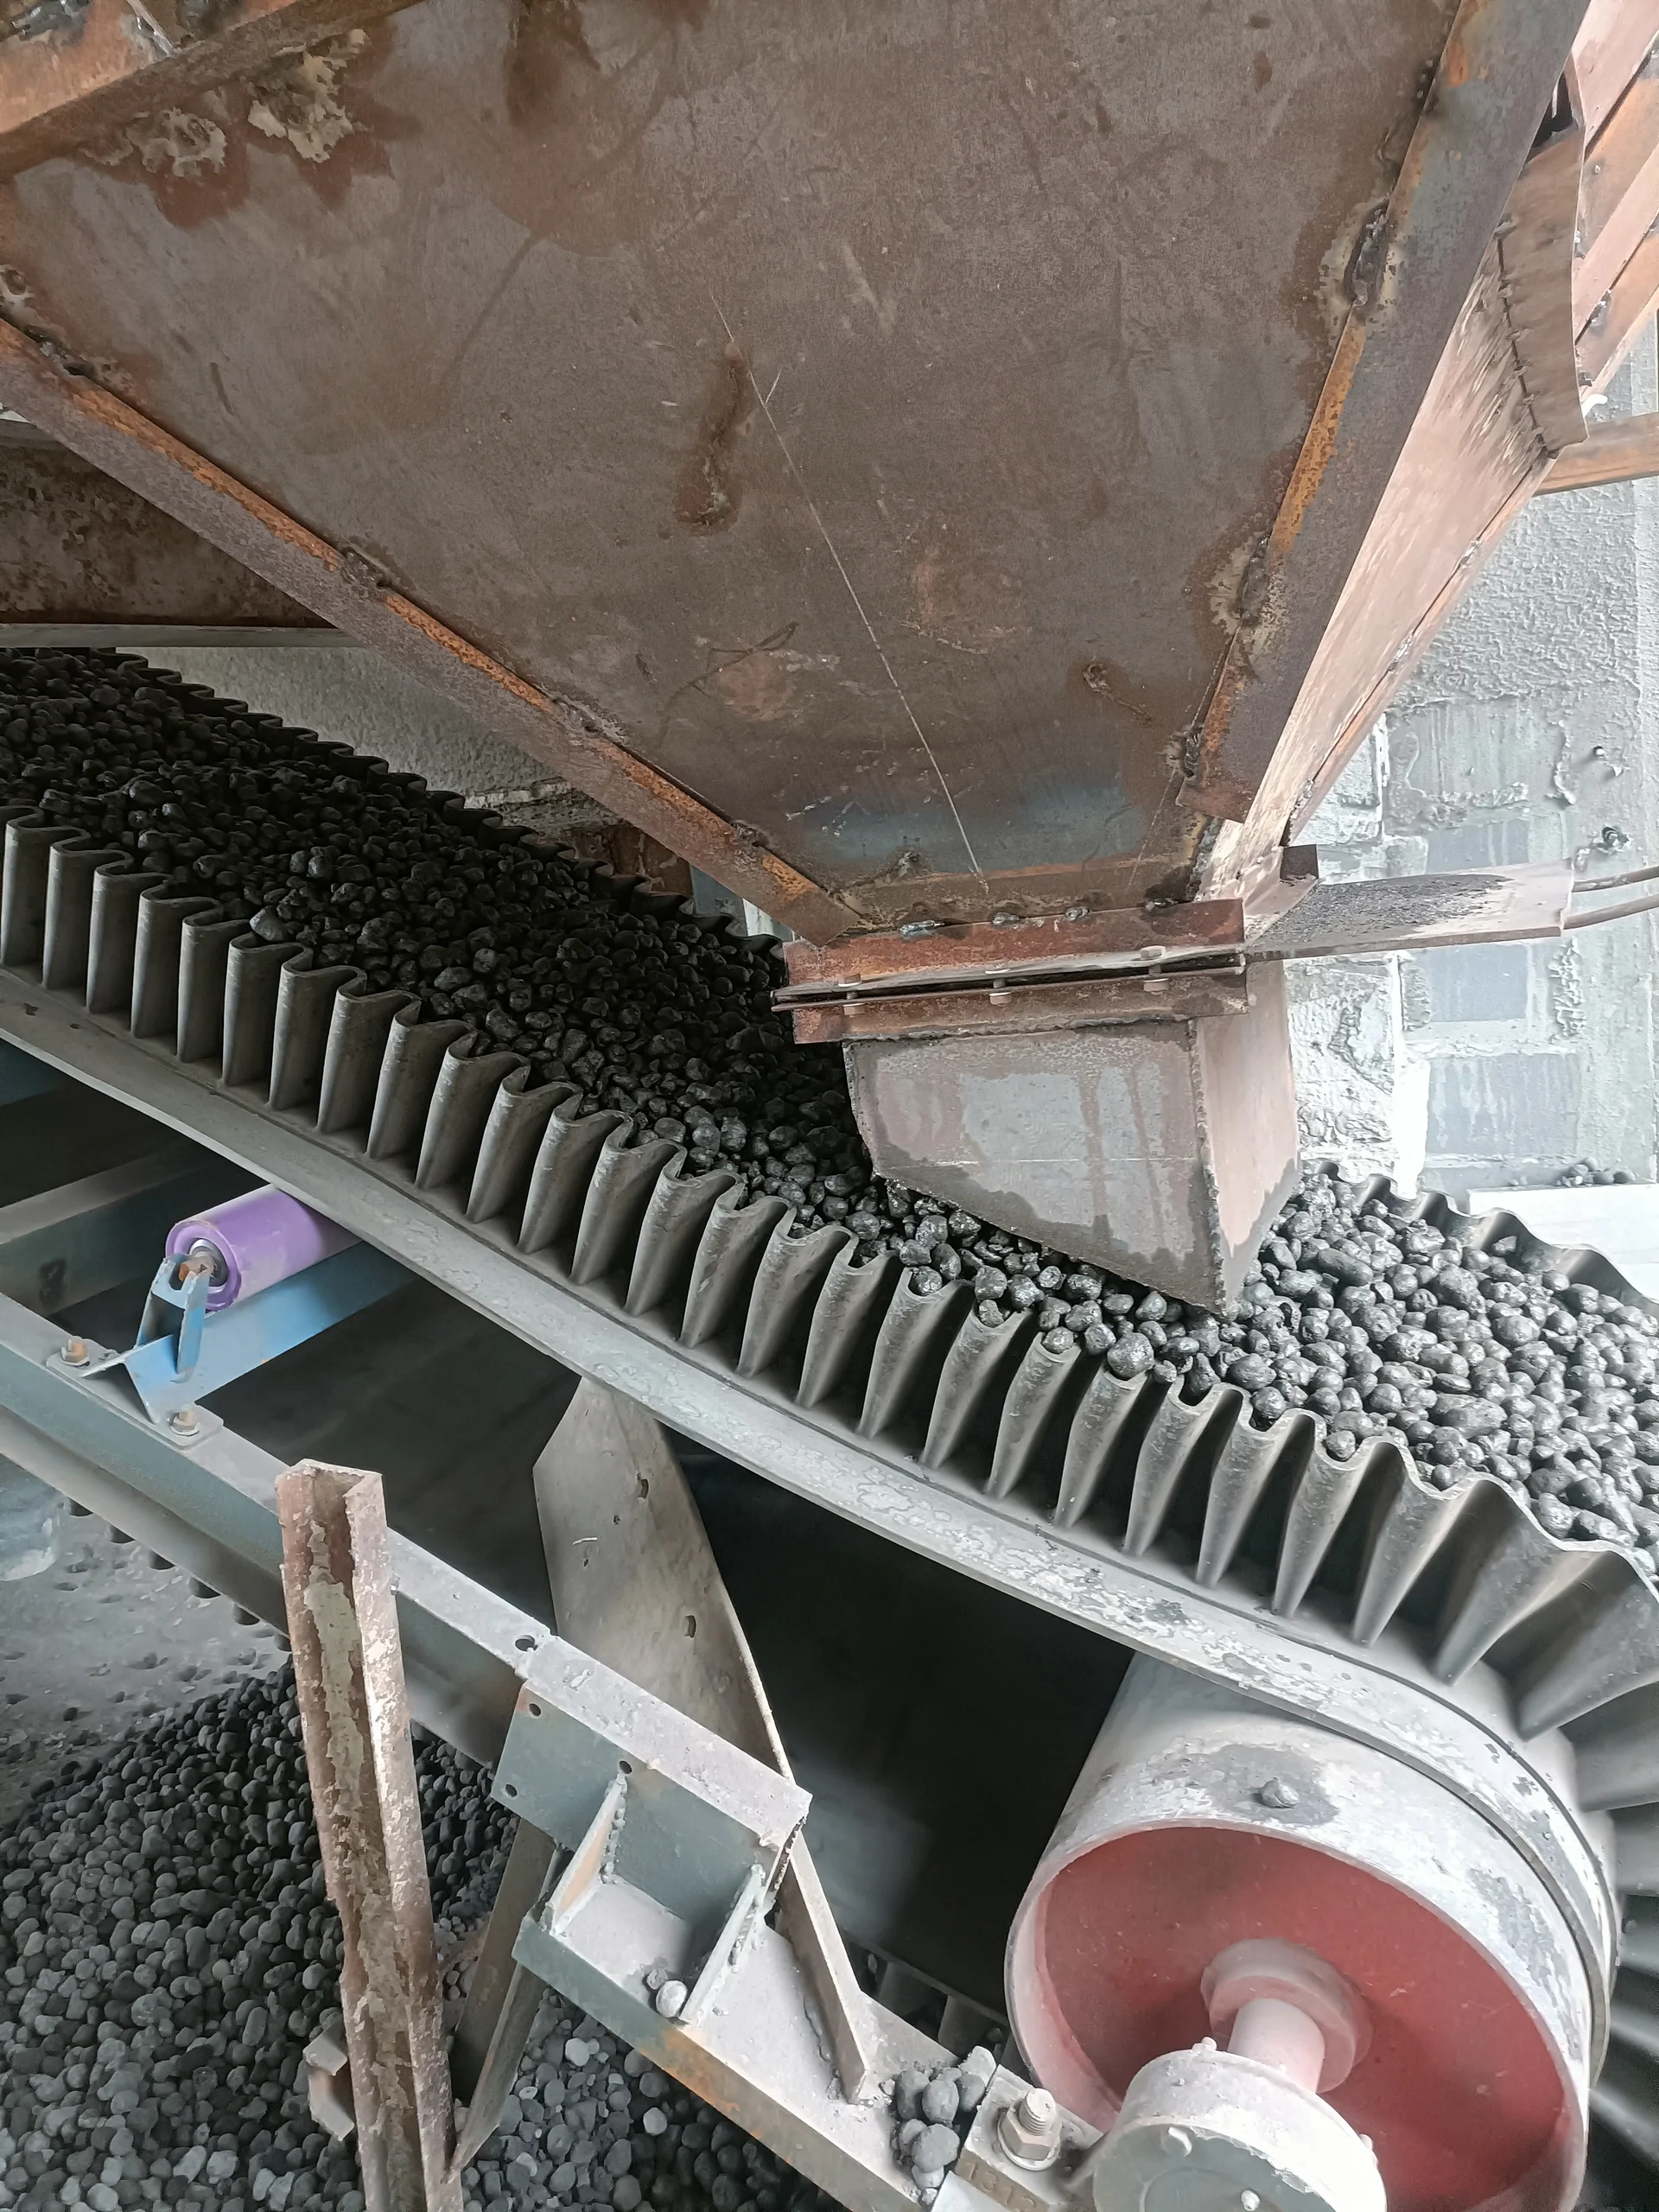
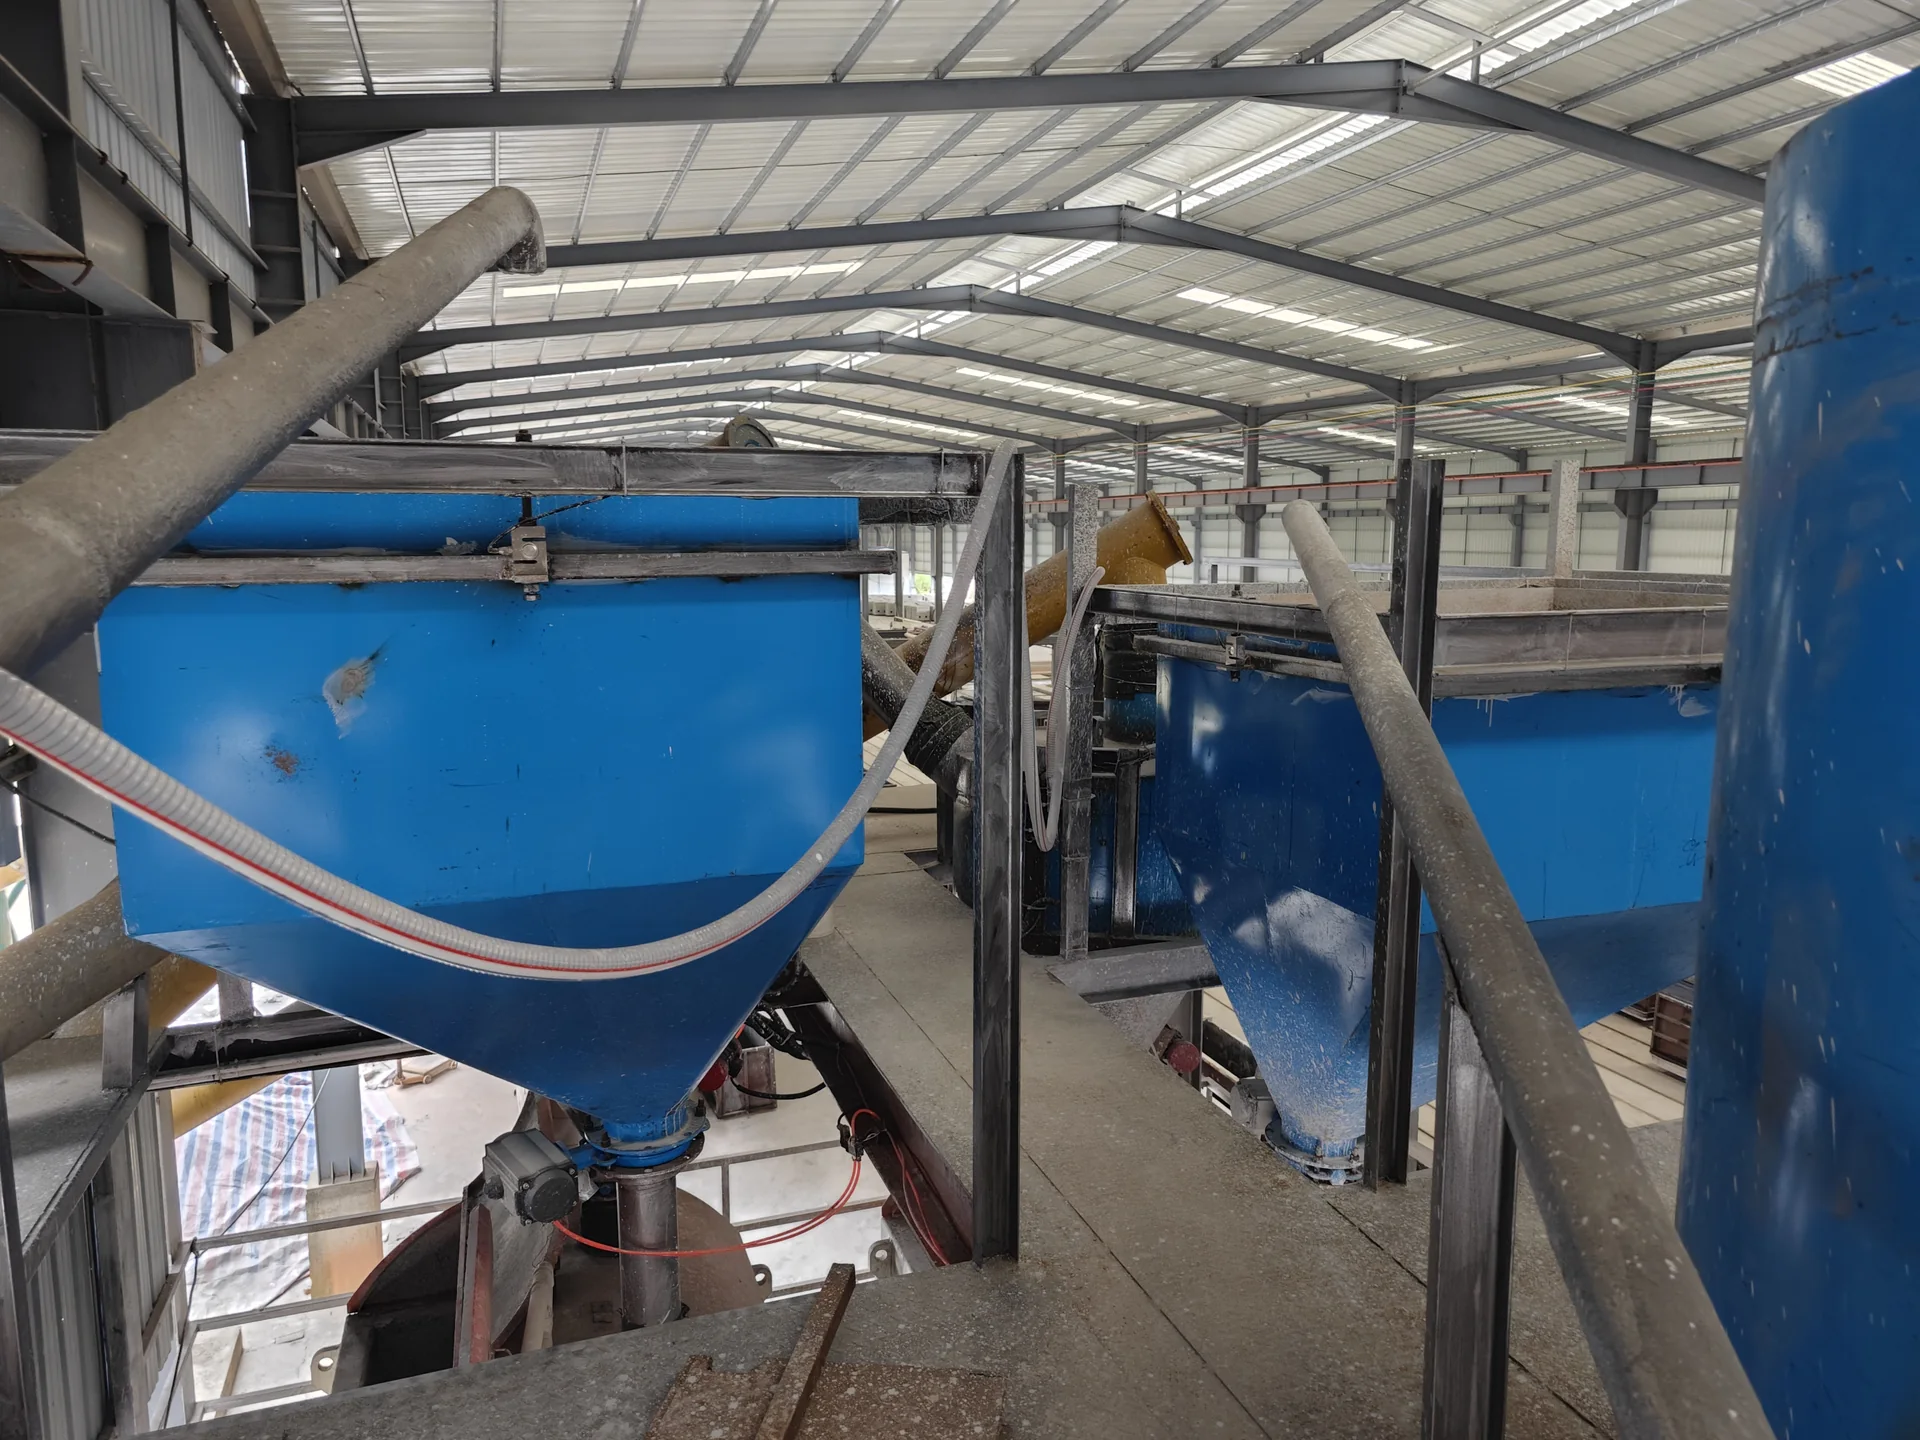
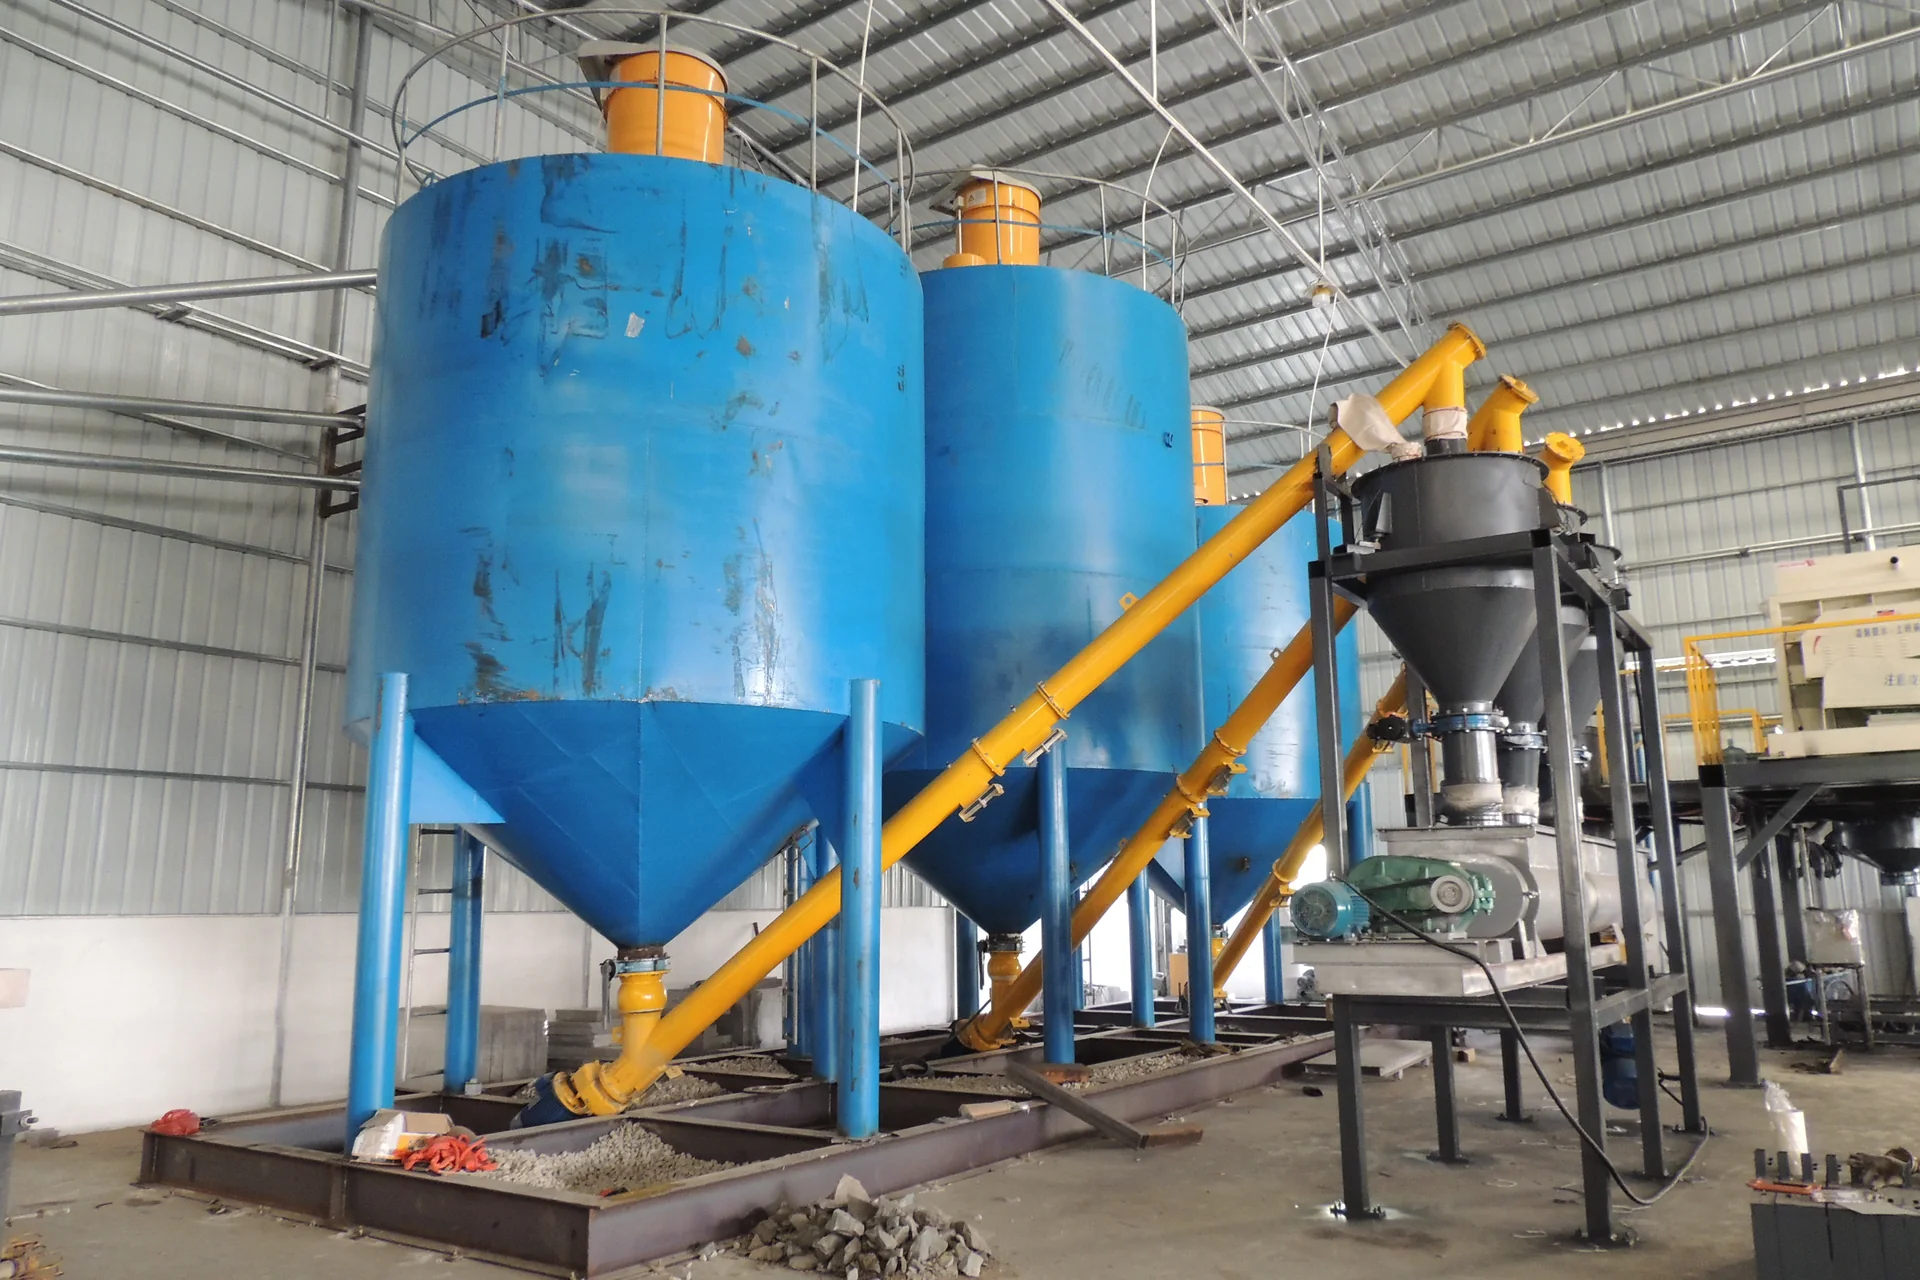
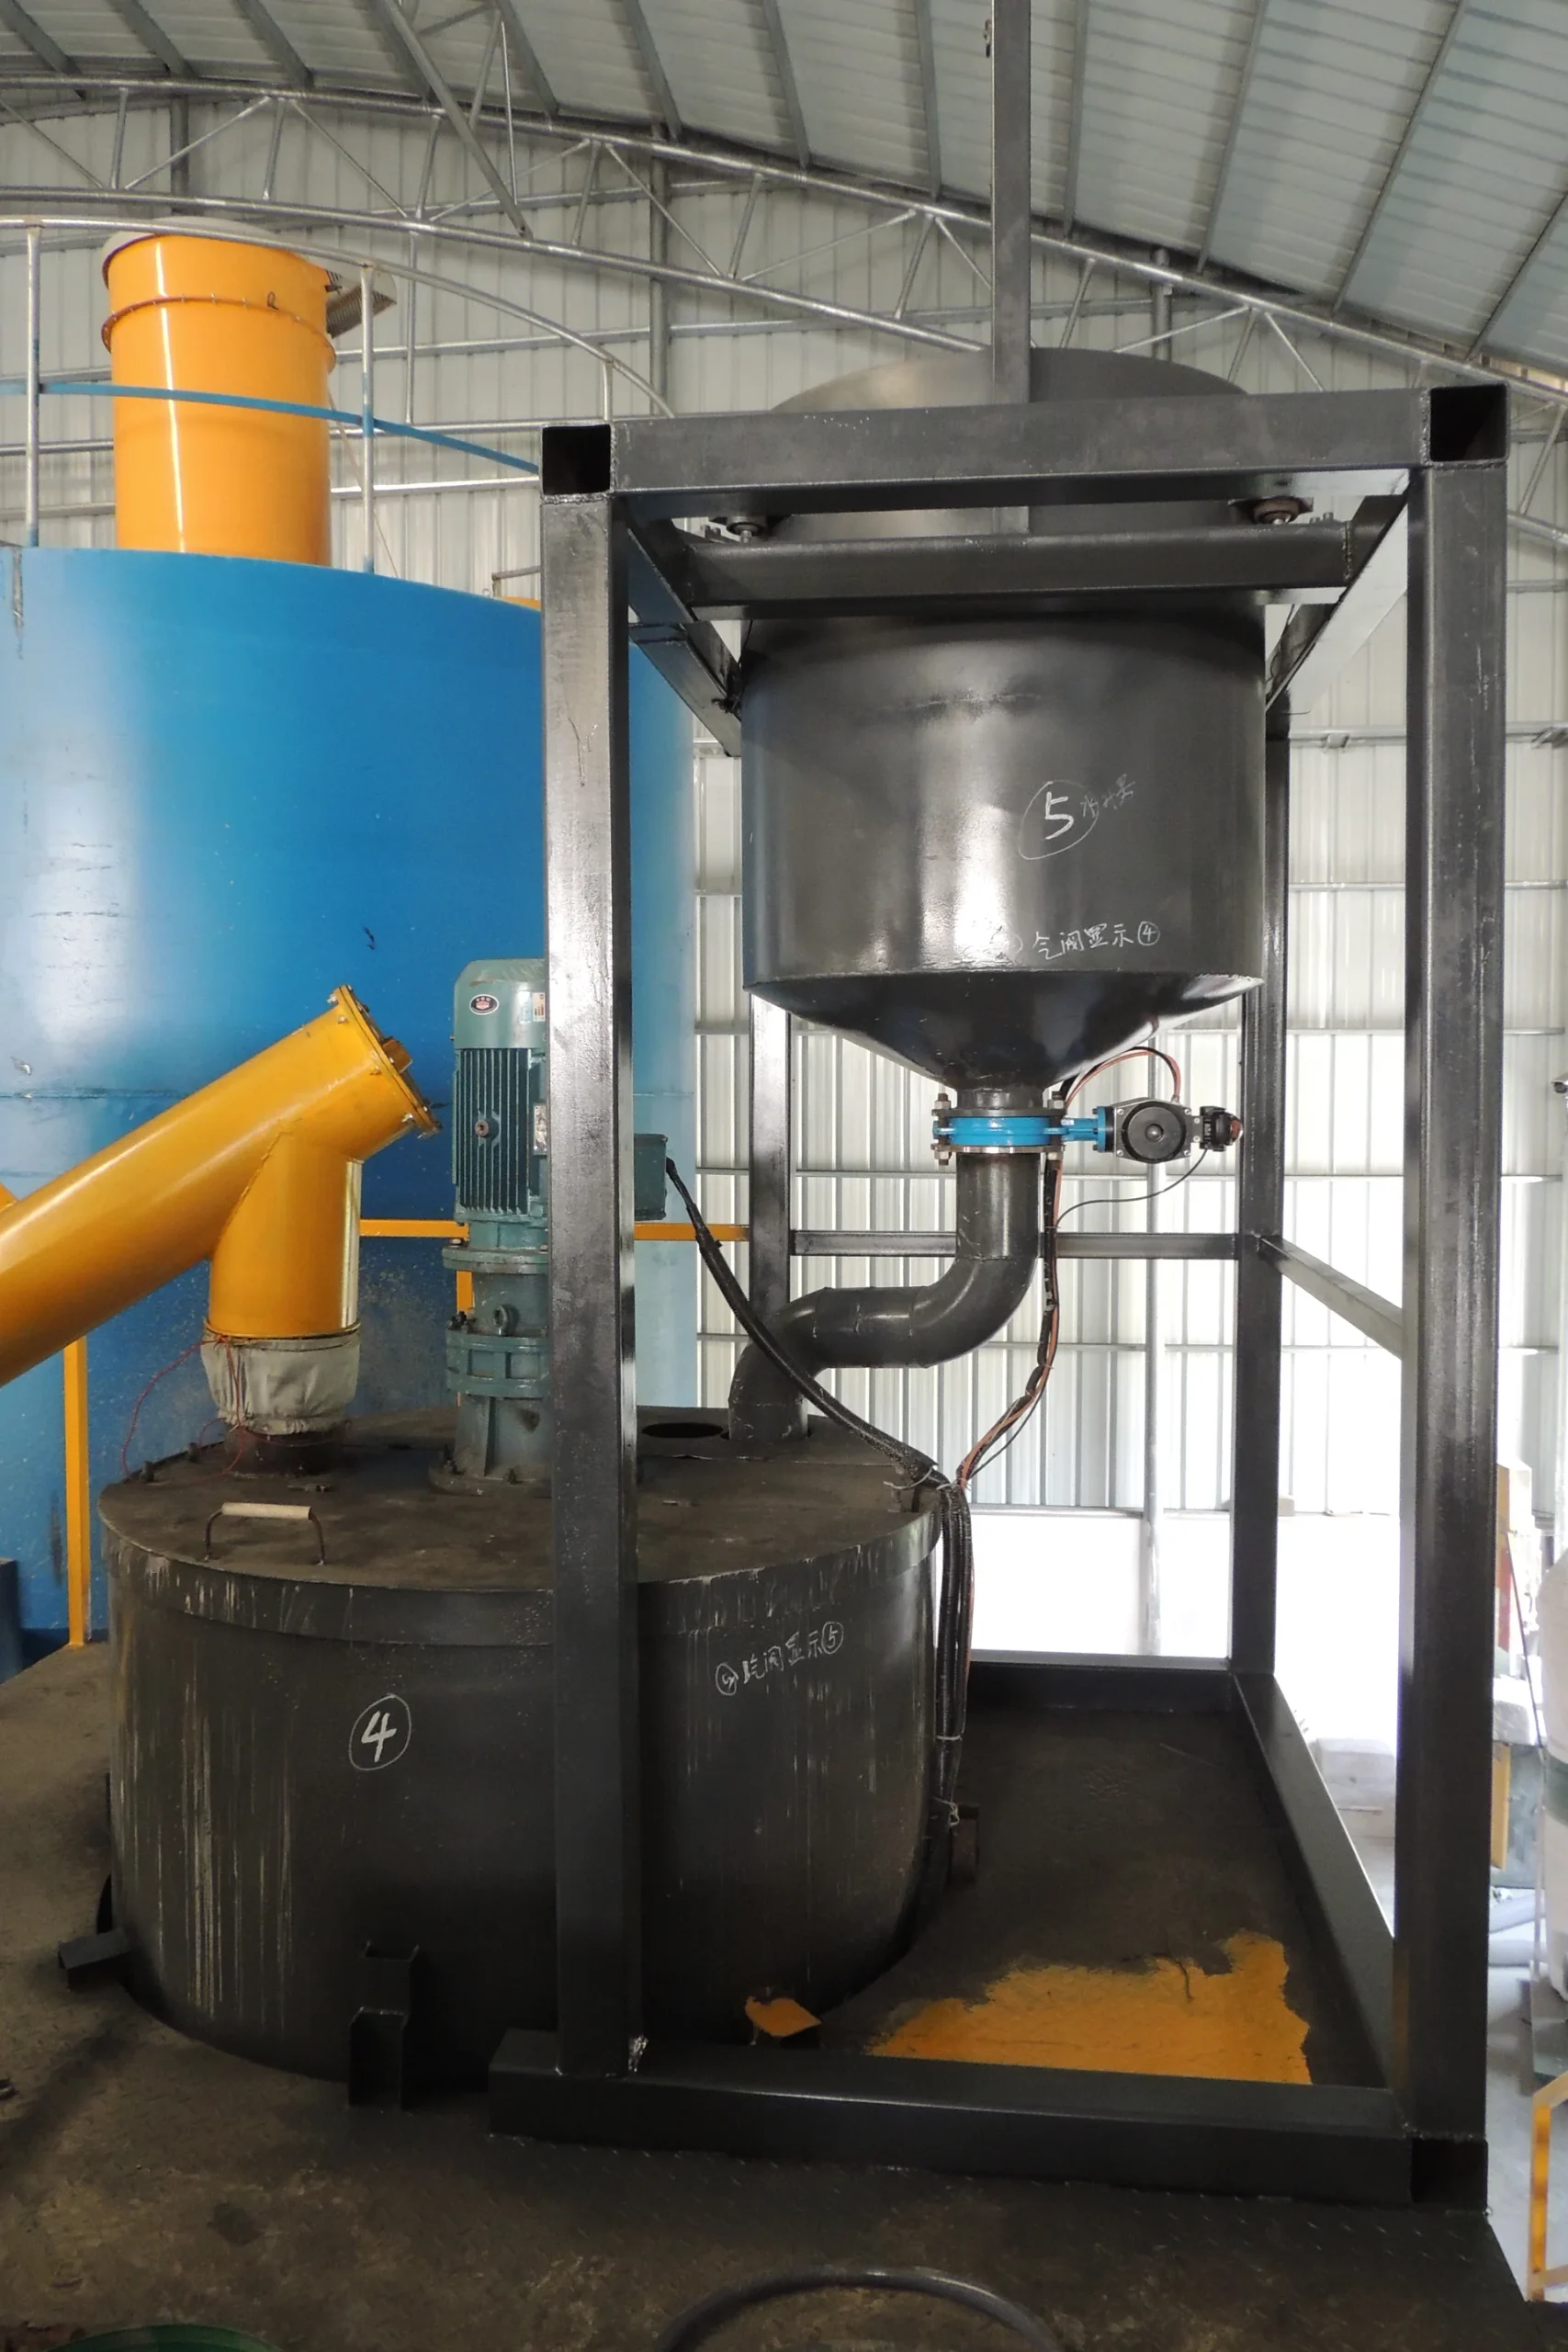
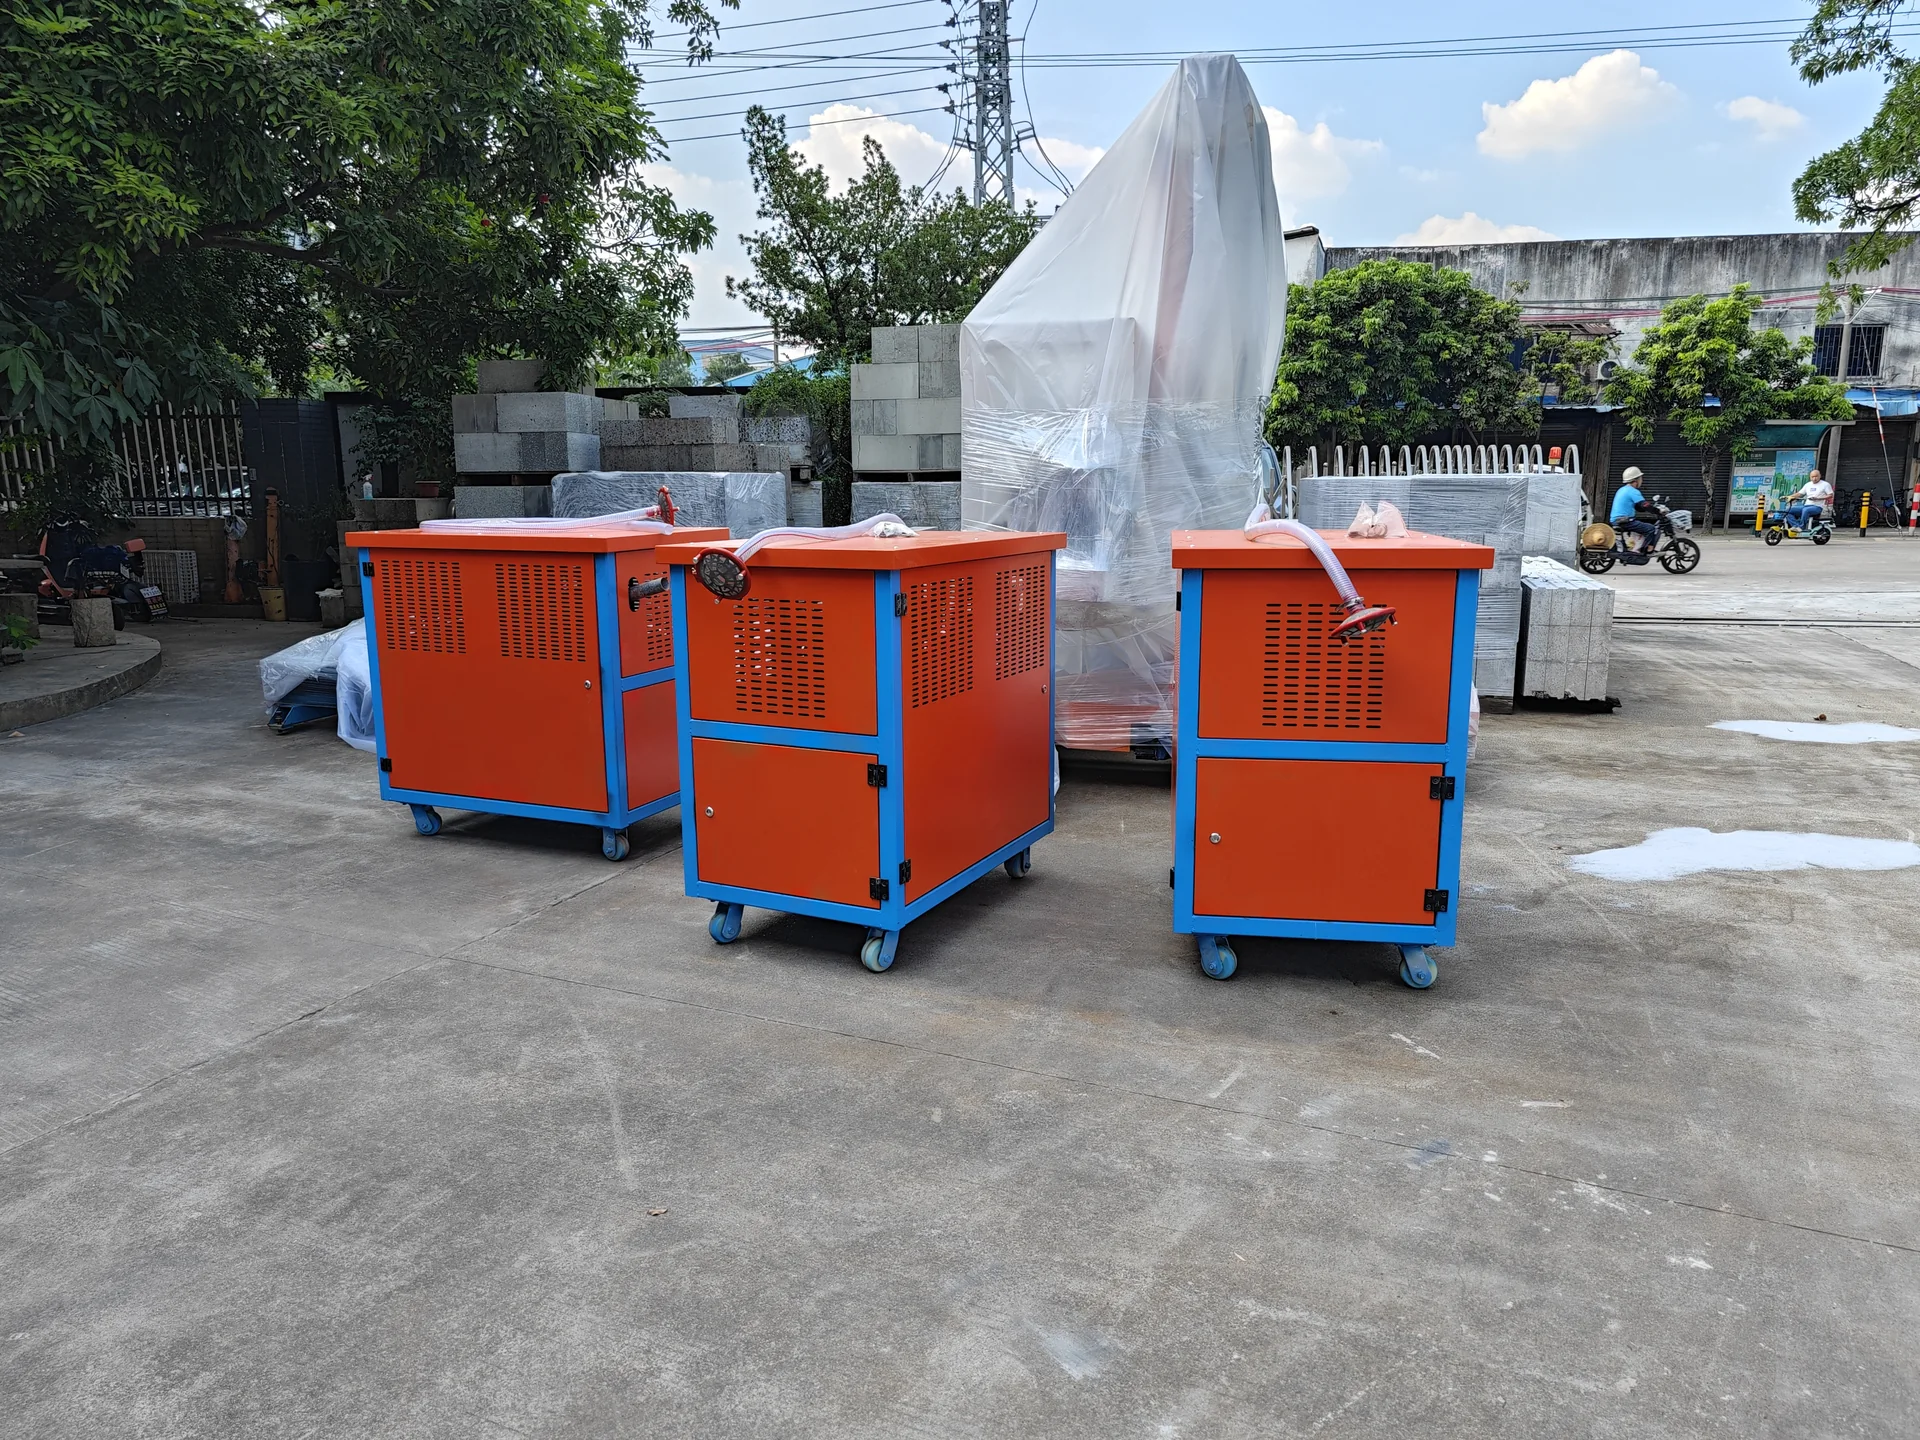
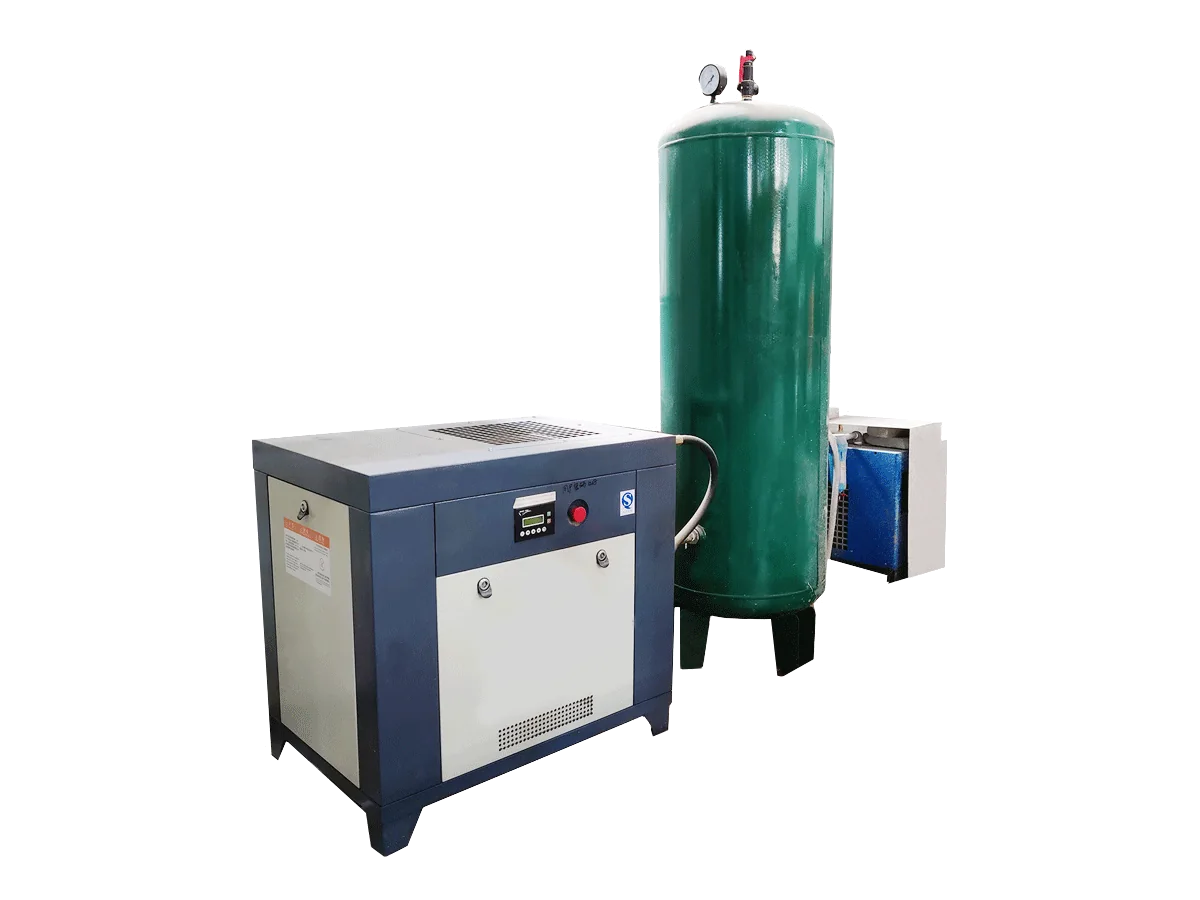
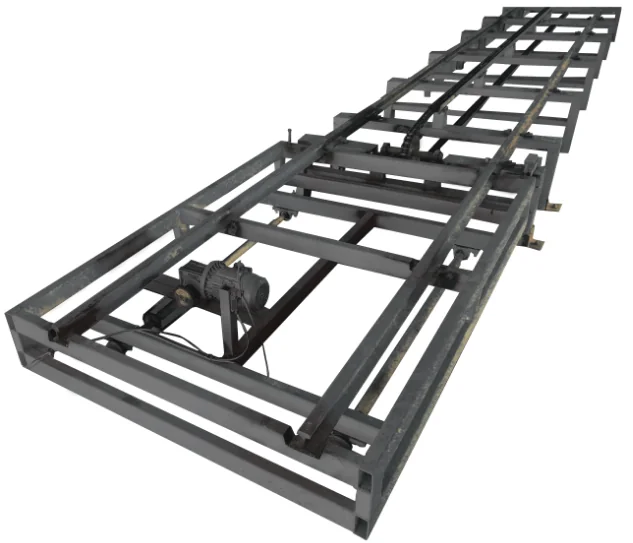
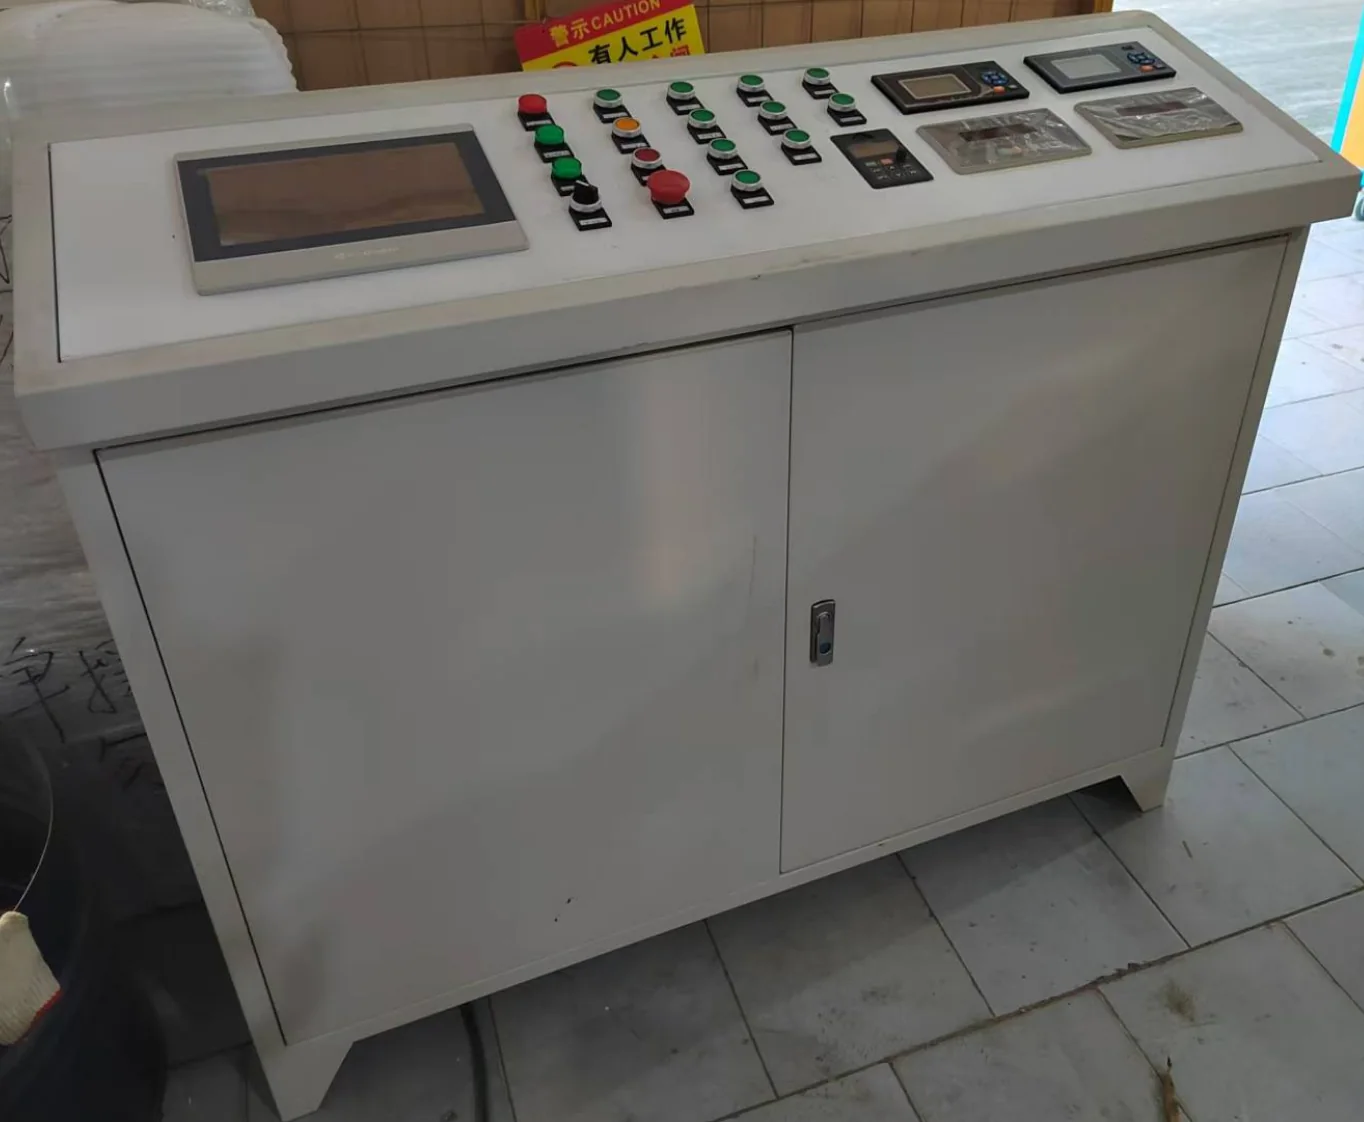
Review the equipment for each production stage. Select an equipment image to enlarge it, or open a linked equipment name for more detail.
Reference mould specification shown: 1 set. Total production mould quantity is calculated separately according to mould volume, curing time and shift plan.
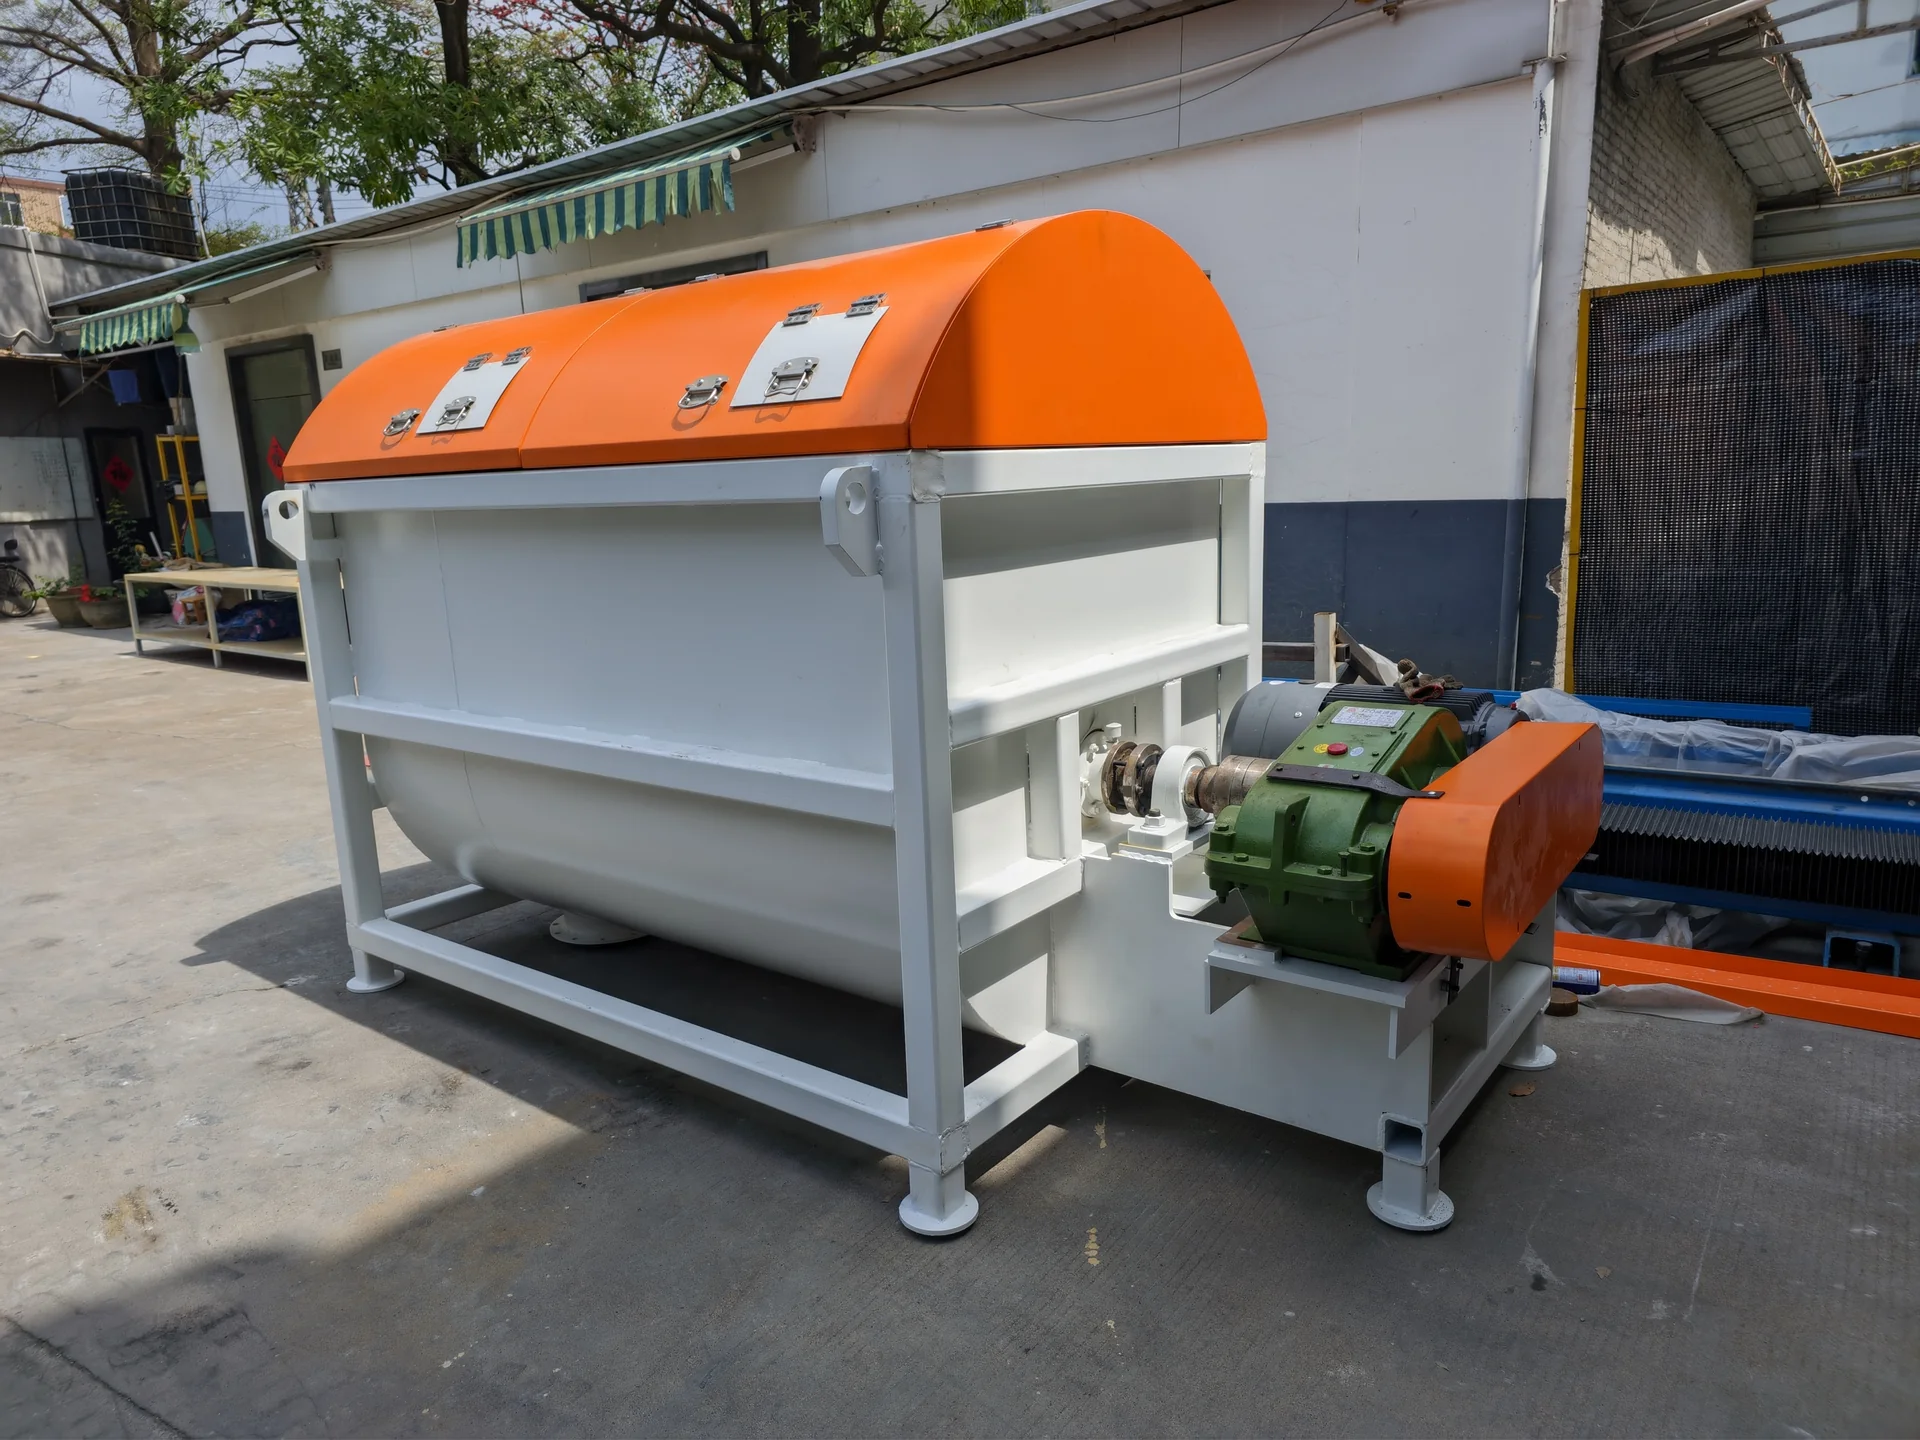
| No. | Equipment | Stage | Model | Dimensions | Qty. | Unit power | Total power (kW) |
|---|---|---|---|---|---|---|---|
| Preparation & metering | |||||||
| 1 | Preparation & metering | HDSL-001 | 8640 × 350 × 1100 | 1 | 11 kW | 11 kW | |
| 2 | Preparation & metering | HDKJ-001 | 18000 × 800 × 800 | 1 | 2.2 kW | 2.2 kW | |
| 3 | Preparation & metering | HDFL-001 | Ø1310 × H1950 | 1 | 0.55 kW | 0.55 kW | |
| 4 | Preparation & metering | HDFL-001 | 1.2 m × 1.5 m × 1.4 m | 1 | 0.55 kW | 0.55 kW | |
| 5 | Preparation & metering | HDSL-001 | Ø1100 × H1140 | 1 | 0.55 kW | 0.55 kW | |
| Physical foaming & mixing | |||||||
| 6 | Physical foaming & mixing | HDKWF1-001 | 1150 × 750 × 1140 | 1 | 7.5 kW | 7.5 kW | |
| 7 | Physical foaming & mixing | HDKY-001 | L1500 × W500 × H2000 mm, air receiver0.8 m³*1 | 1 | 15 kW | 15 kW | |
| Preparation & metering | |||||||
| 8 | Preparation & metering | — | 5000 × 3500 × 1500 | 1 | — | — | |
| Physical foaming & mixing | |||||||
| 9 | Physical foaming & mixing | EPSJB-01 | 1.5 m³ | 1 | 22 kW | 22 kW | |
| Preparation & metering | |||||||
| 10 | Minor-material metering system | Preparation & metering | — | — | 1 | — | — |
| Handling & stacking | |||||||
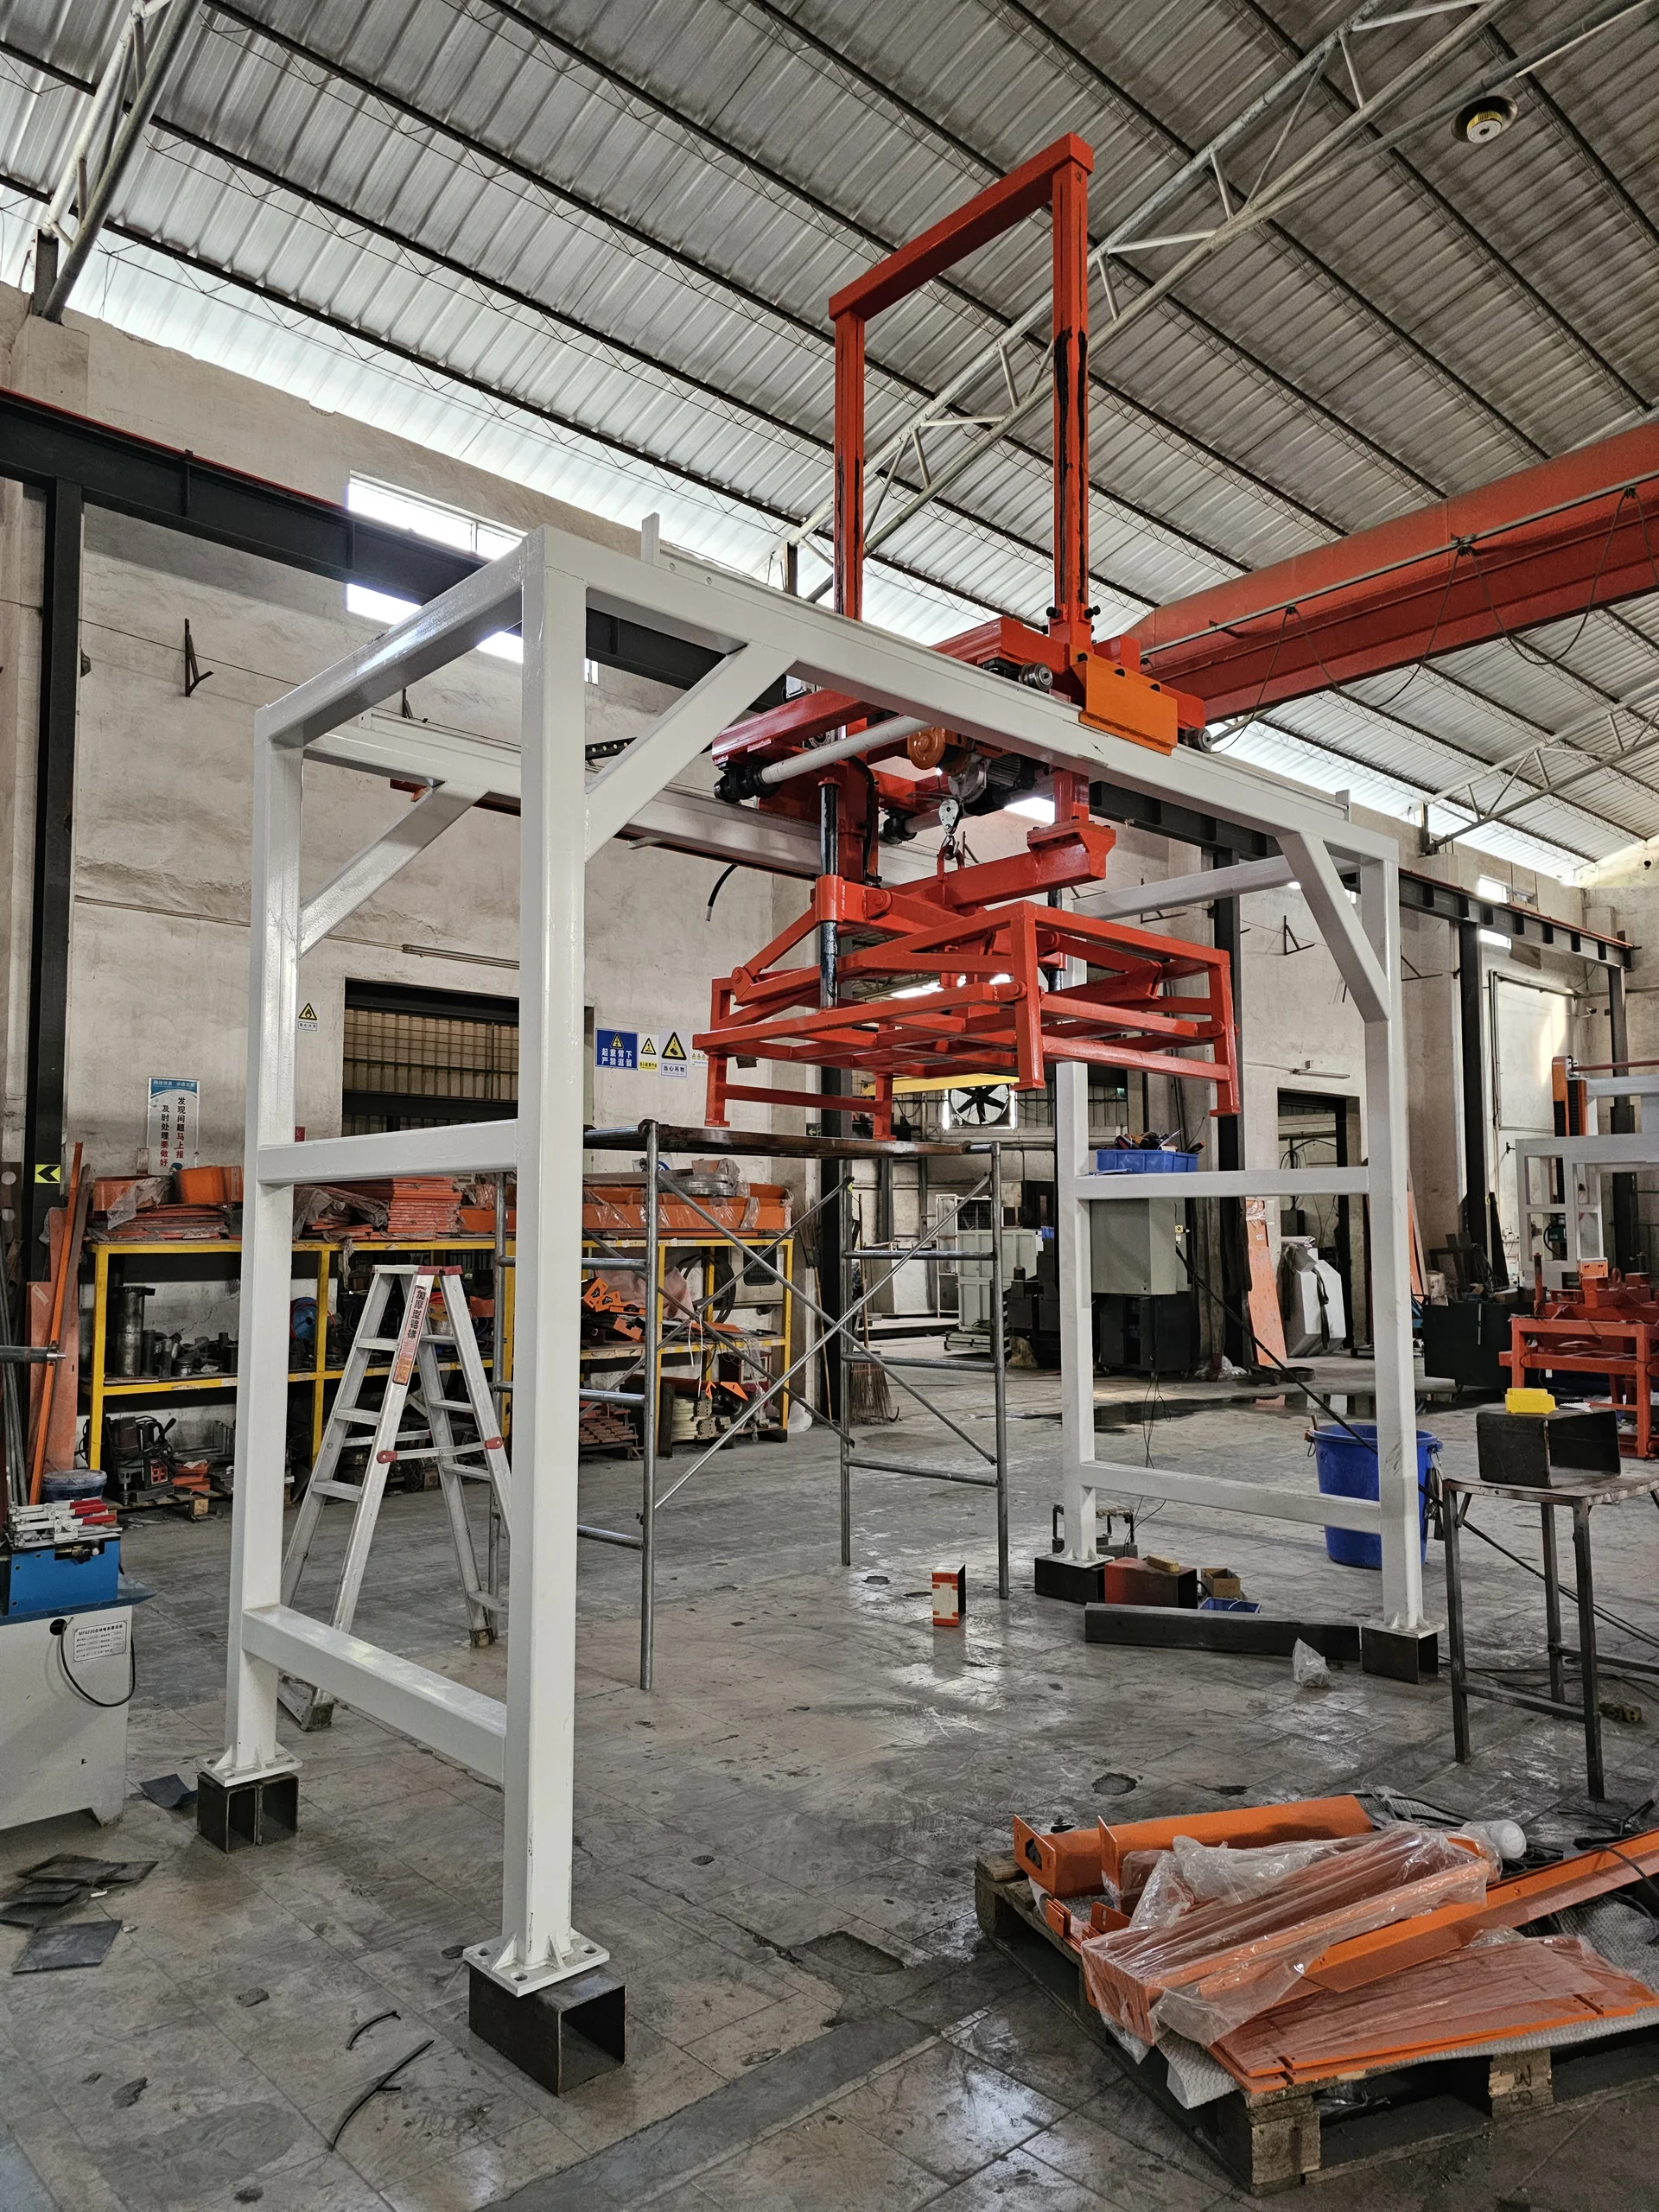
| 11 | Handling & stacking | HDKHG-001 | 4.9 m × 2.8 m × 4.2 m | 1 | 5 kW | 5 kW | |
| Cutting & finishing | |||||||
| 12 | Cutting & finishing | HDOSD1-001 | 3000*1000*2100 (including powered line) | 1 | 22 kW | 22 kW | |
| Handling & stacking | |||||||
| 13 | Handling & stacking | HDTH-005 | 2430 × 1330 × 3900 | 1 | 7.5 kW | 7.5 kW | |
| Cutting & finishing | |||||||
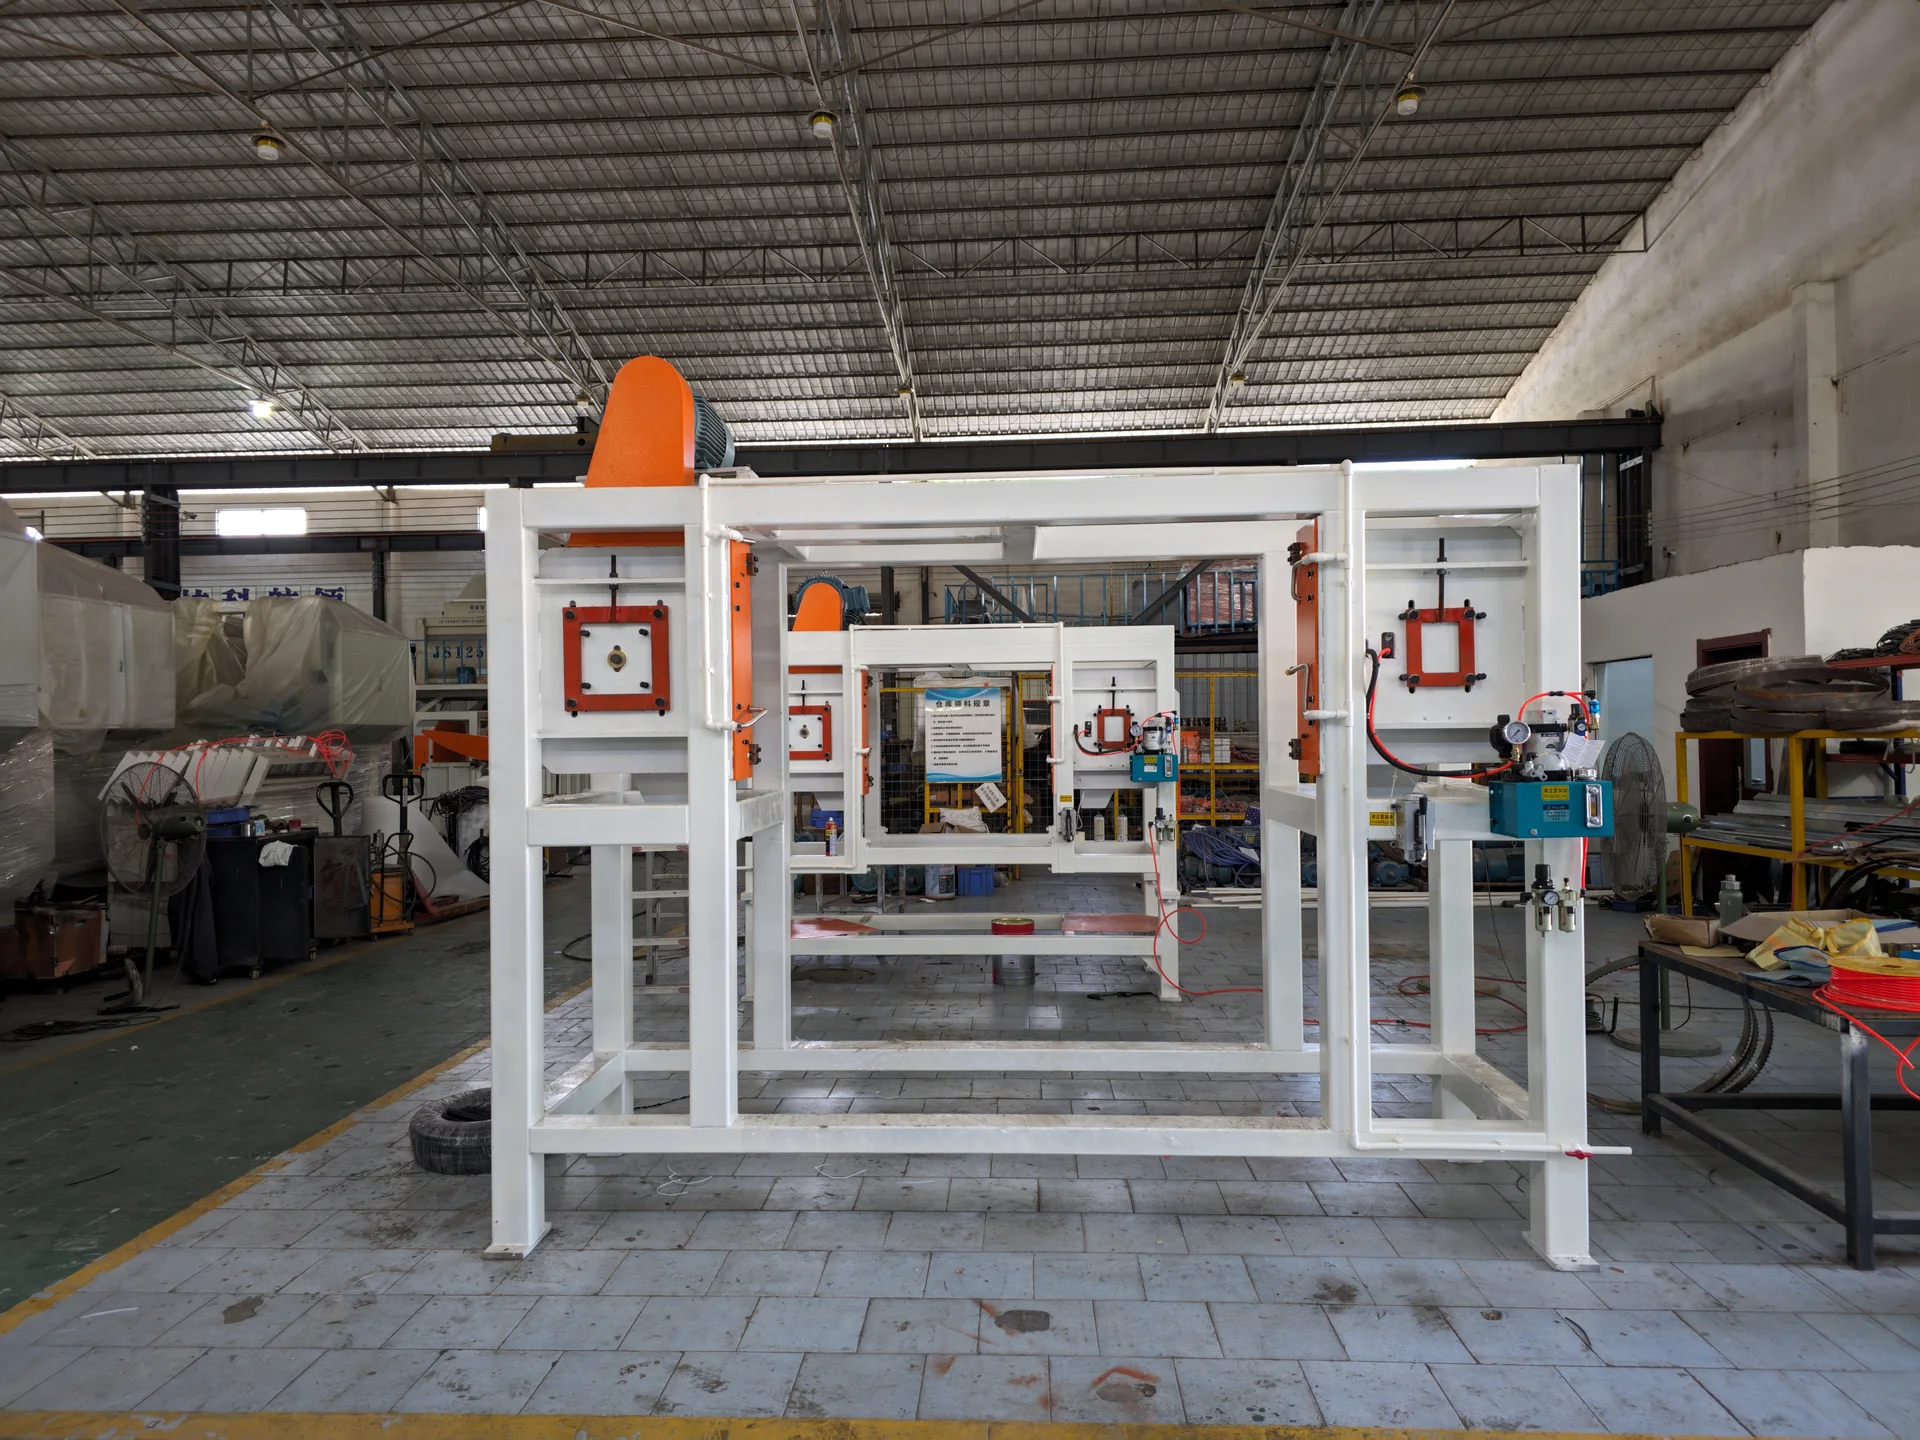
| 14 | Two-station vertical cutter | Cutting & finishing | HDSHM1-001 | 6650 × 3300 × 3650 (high-precision rotary configuration) | 1 | 31.9 kW | 31.9 kW |
| Handling & stacking | |||||||
| 15 | Handling & stacking | HDTH-006 | 4800 × 2600 × 3800 | 1 | 6.2 kW | 6.2 kW | |
| Moulding, curing & circulation | |||||||
| 16 | Moulding, curing & circulation | HDBD2-001 | 1800 × 1080 × 400 | 5 | 3 kW | 15 kW | |
| 17 | Moulding, curing & circulation | TM-001 | 12 m × 1.1 m | 1 | 2.2 kW | 2.2 kW | |
| 18 | Moulding, curing & circulation | HM-001 | 12 m × 1.1 m | 1 | 2.2 kW | 2.2 kW | |
| 19 | Moulding, curing & circulation | JZ-001 | 12 m × 1.1 m | 1 | 2.2 kW | 2.2 kW | |
| 20 | Moulding, curing & circulation | HDZD-001 | 4 m × 1.1 m | 2 | 0.3 kW | 0.6 kW | |
| 21 | Moulding, curing & circulation | HDZD-002 | 4 m × 1.1 m | 2 | 0.3 kW | 0.6 kW | |
| PLC, electrical & tooling | |||||||
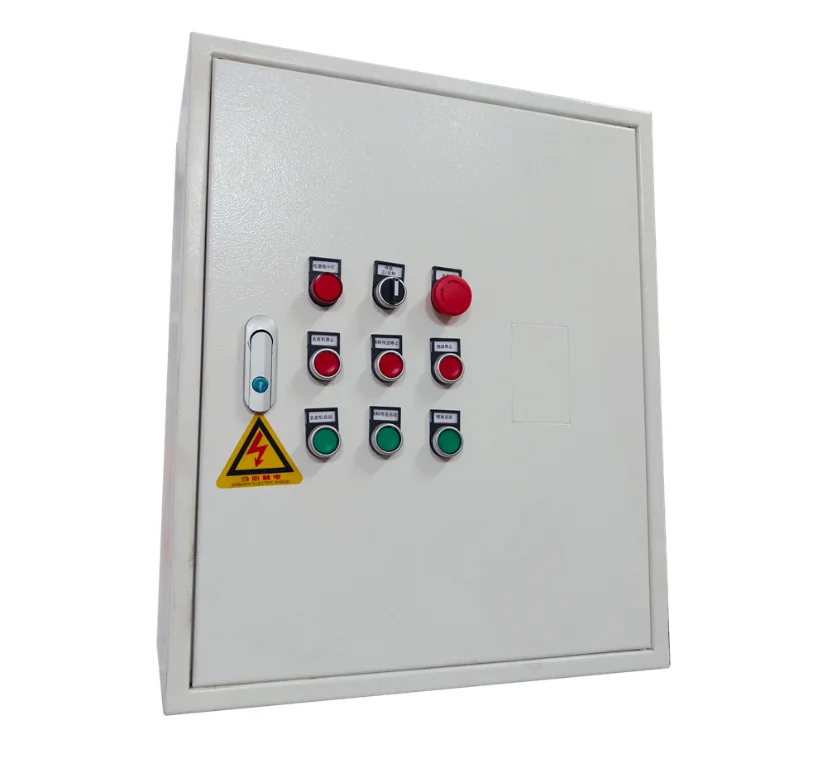
| 22 | PLC, electrical & tooling | HDKZ1-001 | 1300 × 1100 × 400 | 1 | — | — | |
| 23 | PLC, electrical & tooling | HDCBD1-001 | 700 × 500 × 400 | 1 | — | — | |
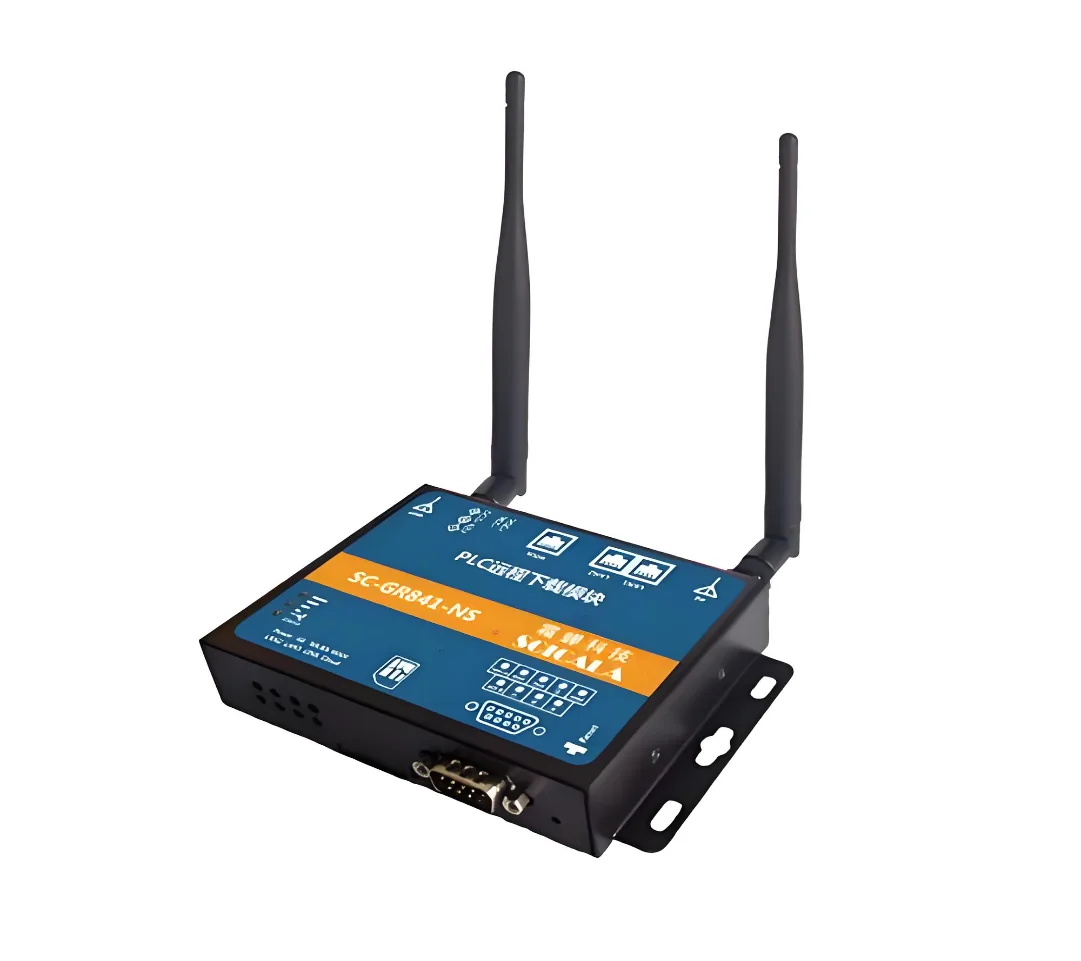
| 24 | PLC, electrical & tooling | — | — | 1 | — | — | |
| PLC, electrical & tooling | |||||||
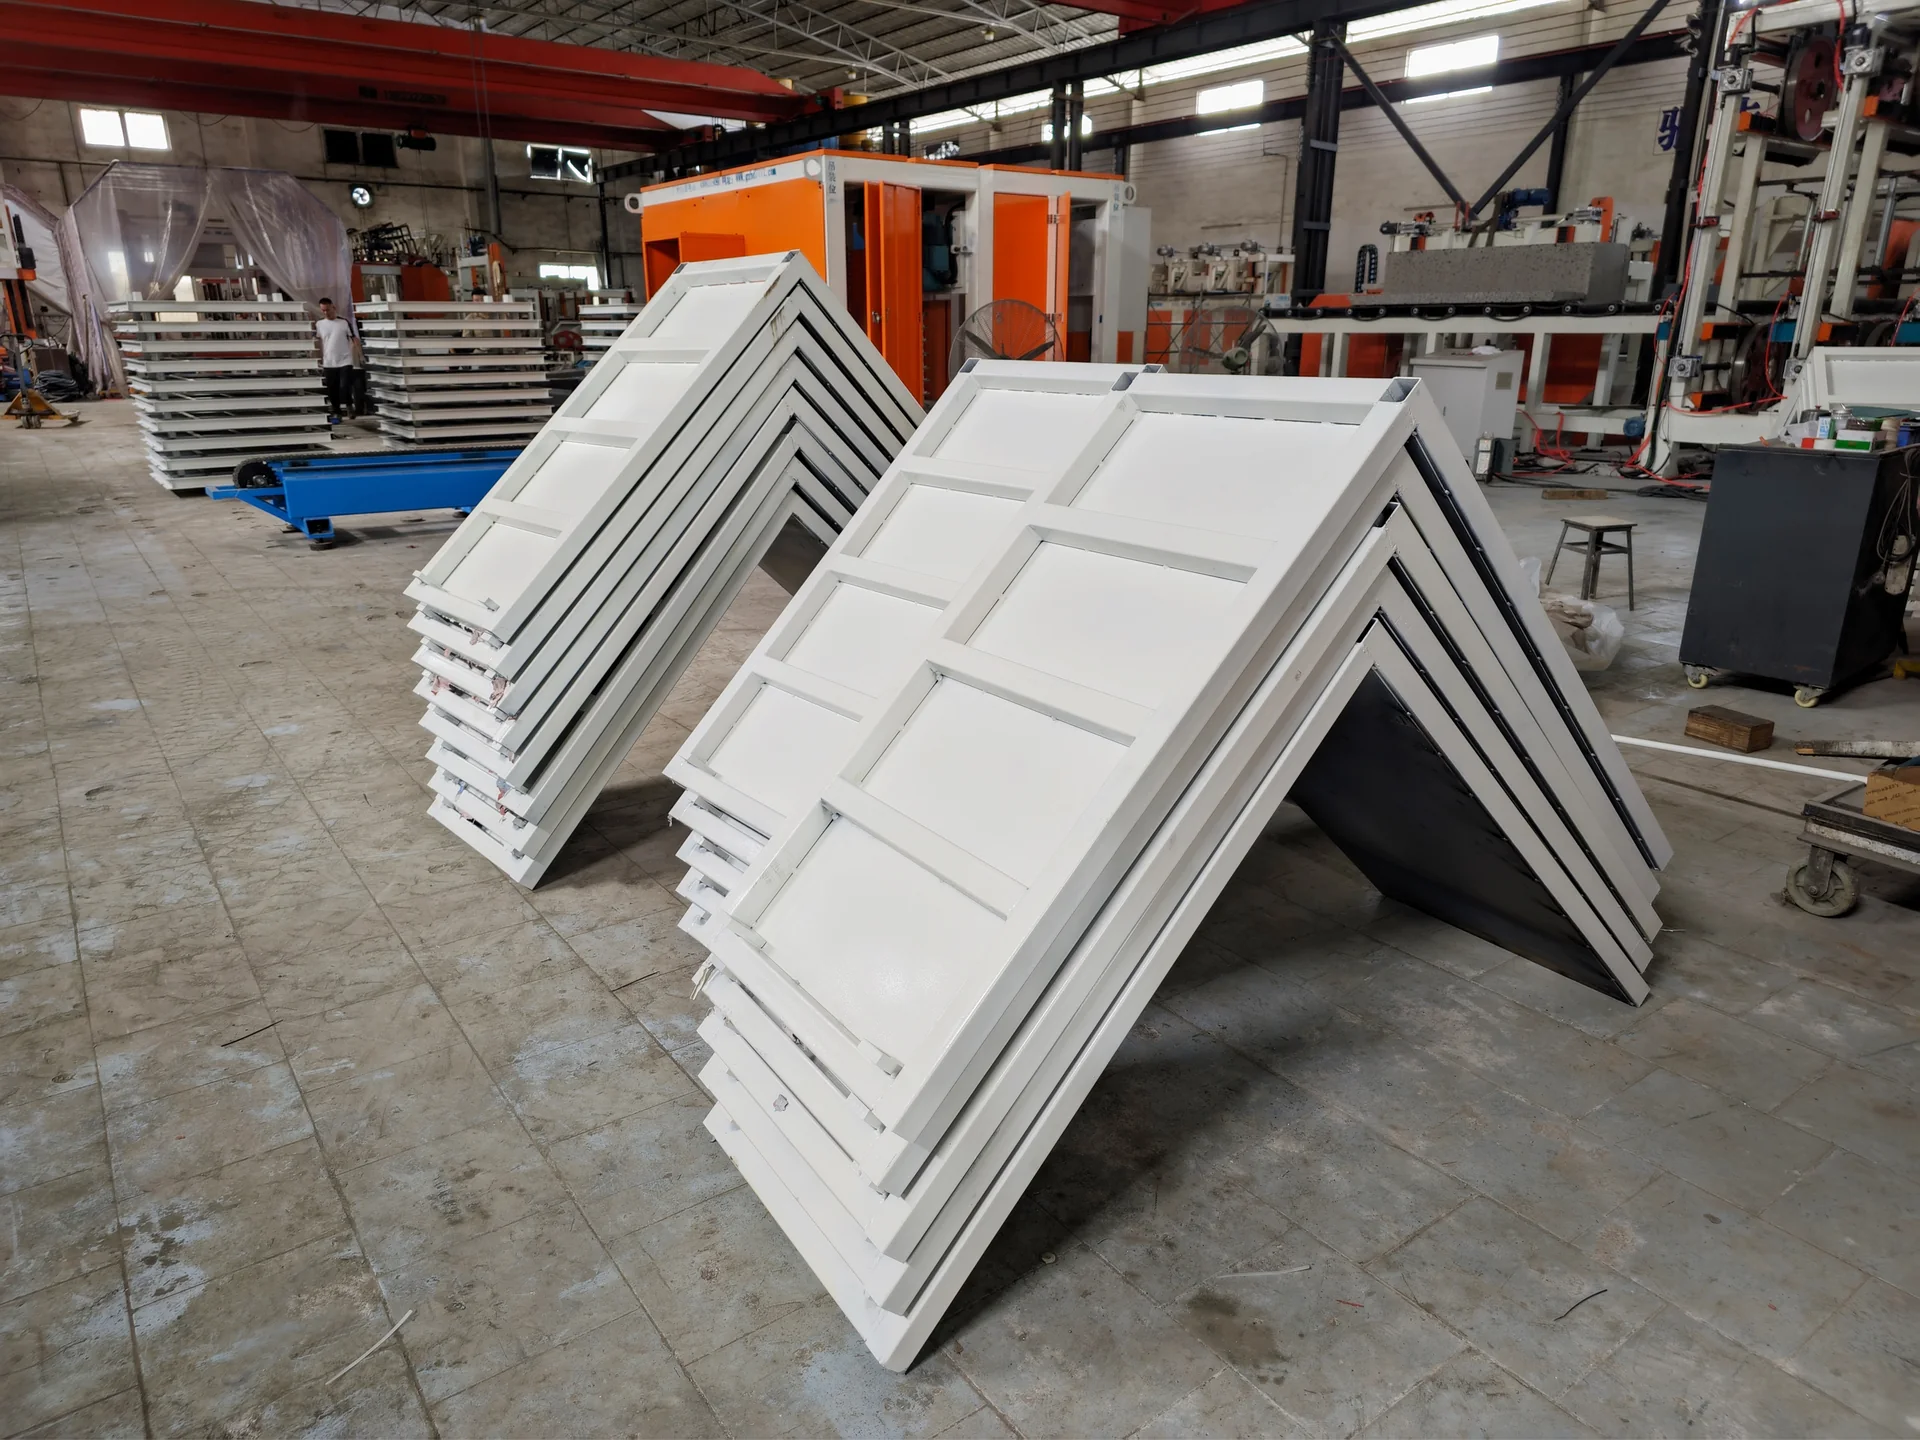
| 25 | Production equipment | HDCM1-002 | 1220 × 1220 × 630 (complete set) | 1 | — | — | |
PRODUCTION LINE GALLERY
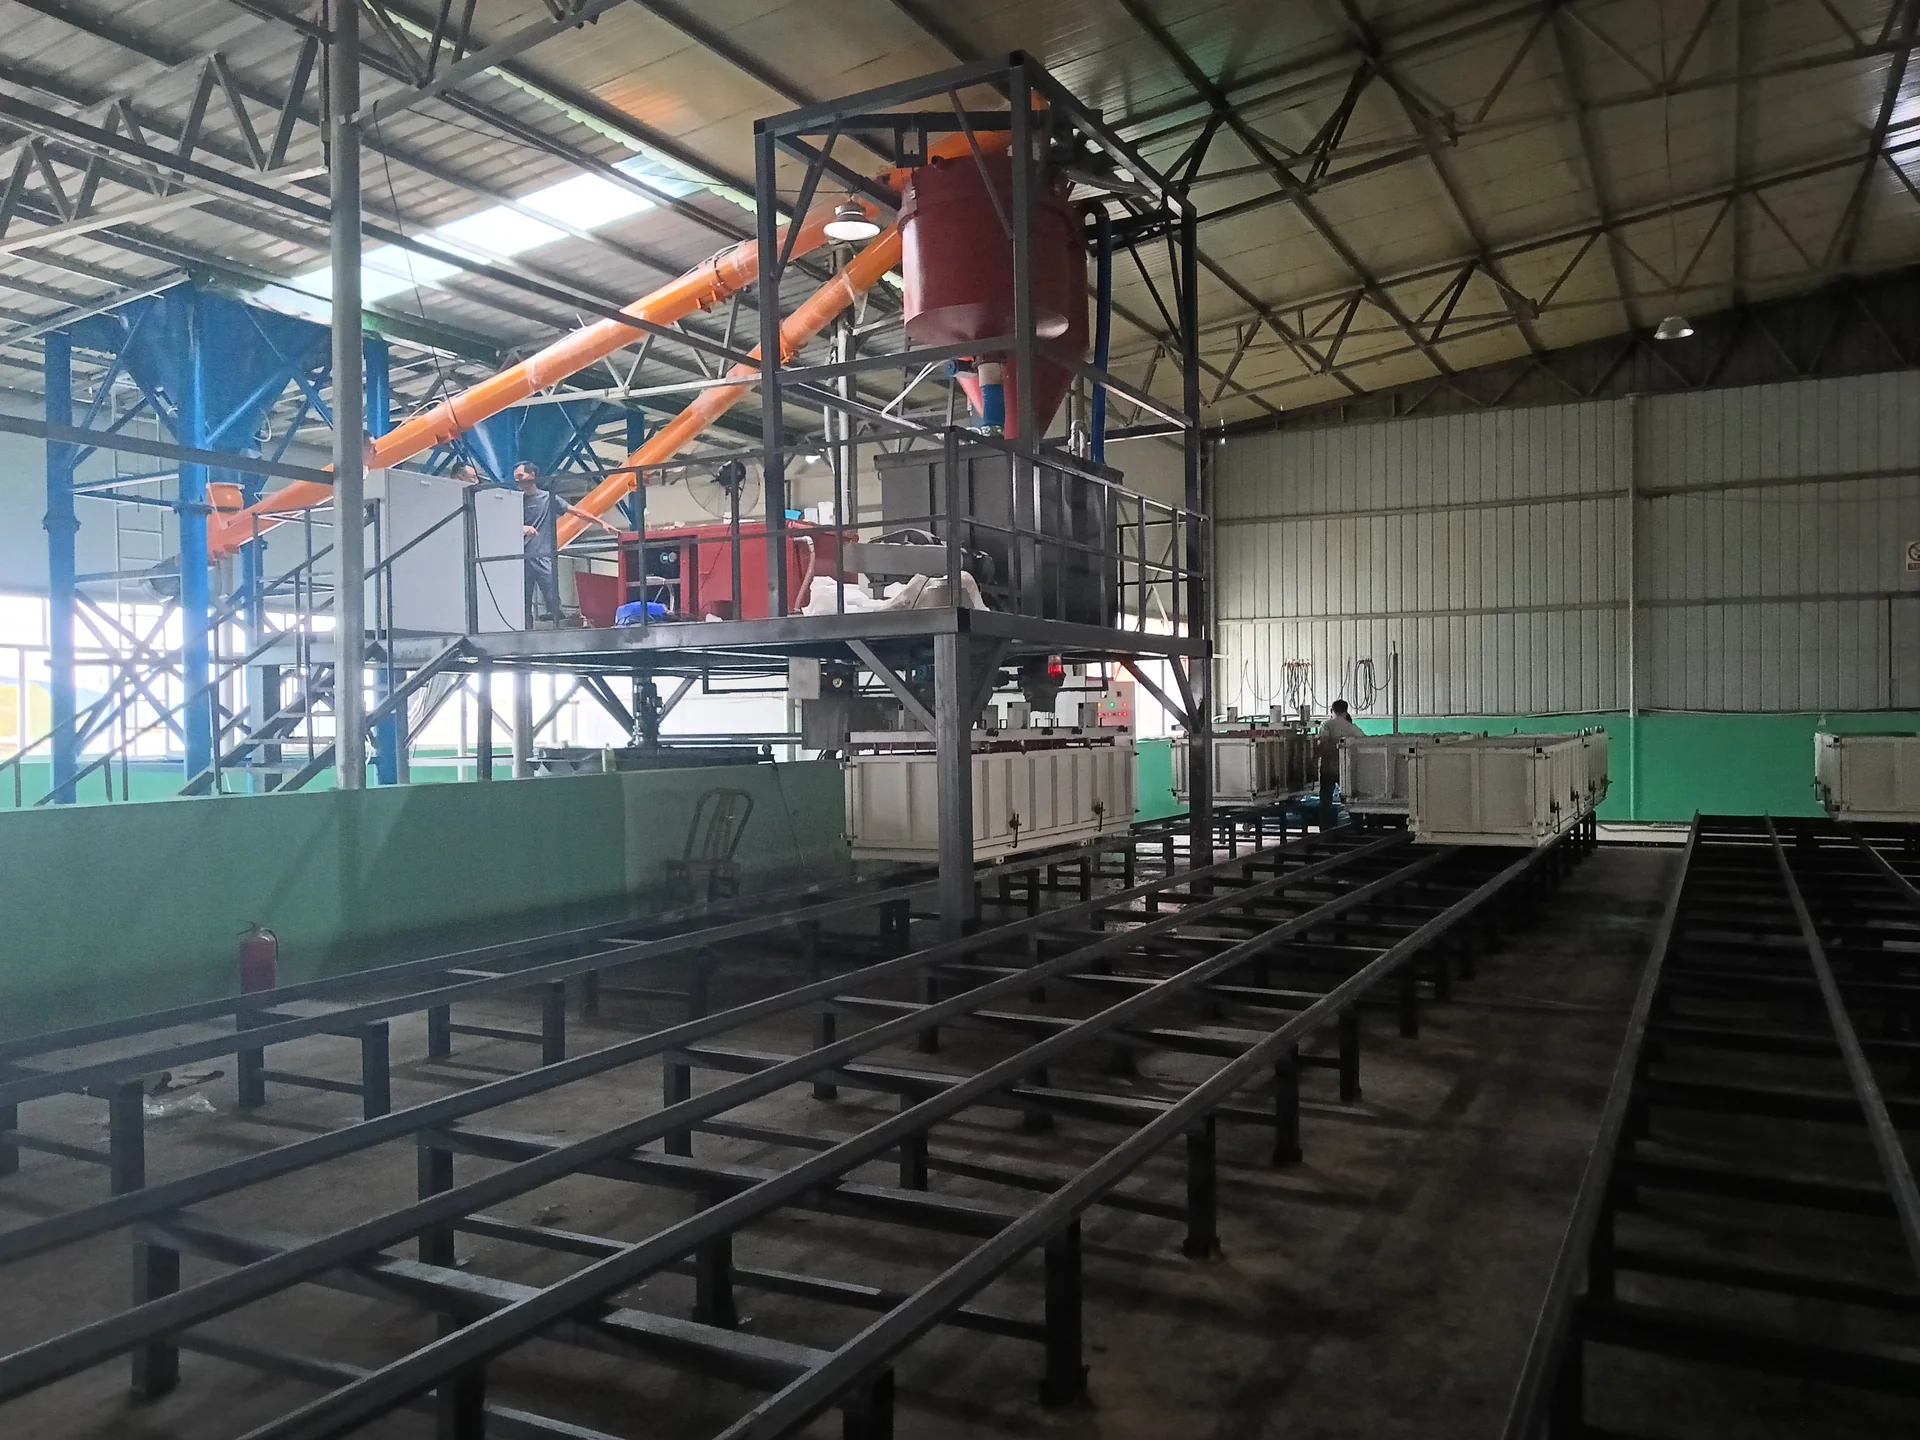
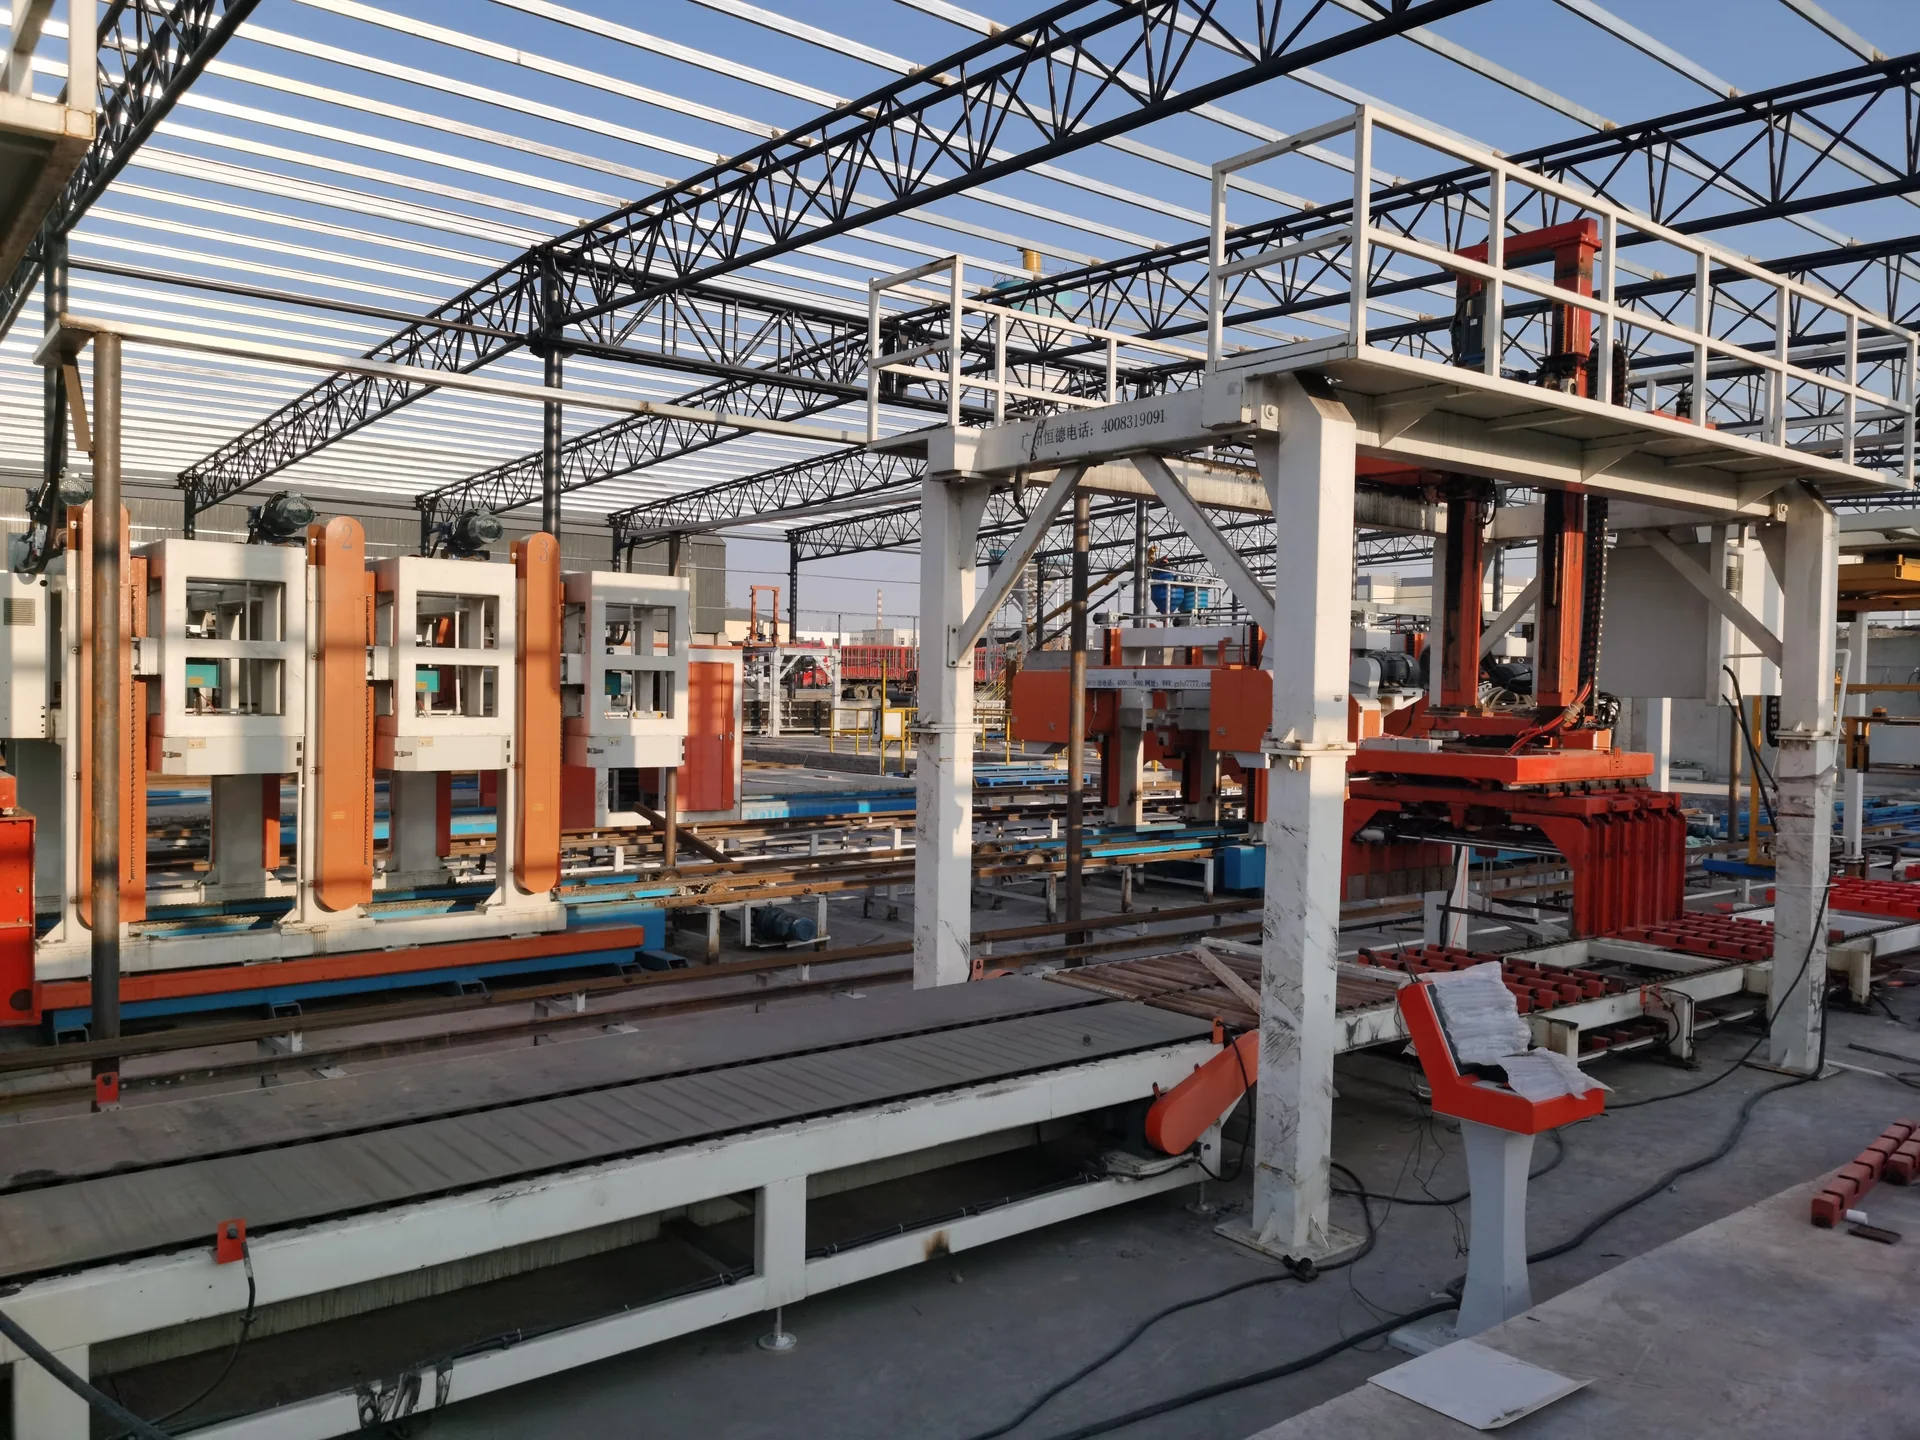
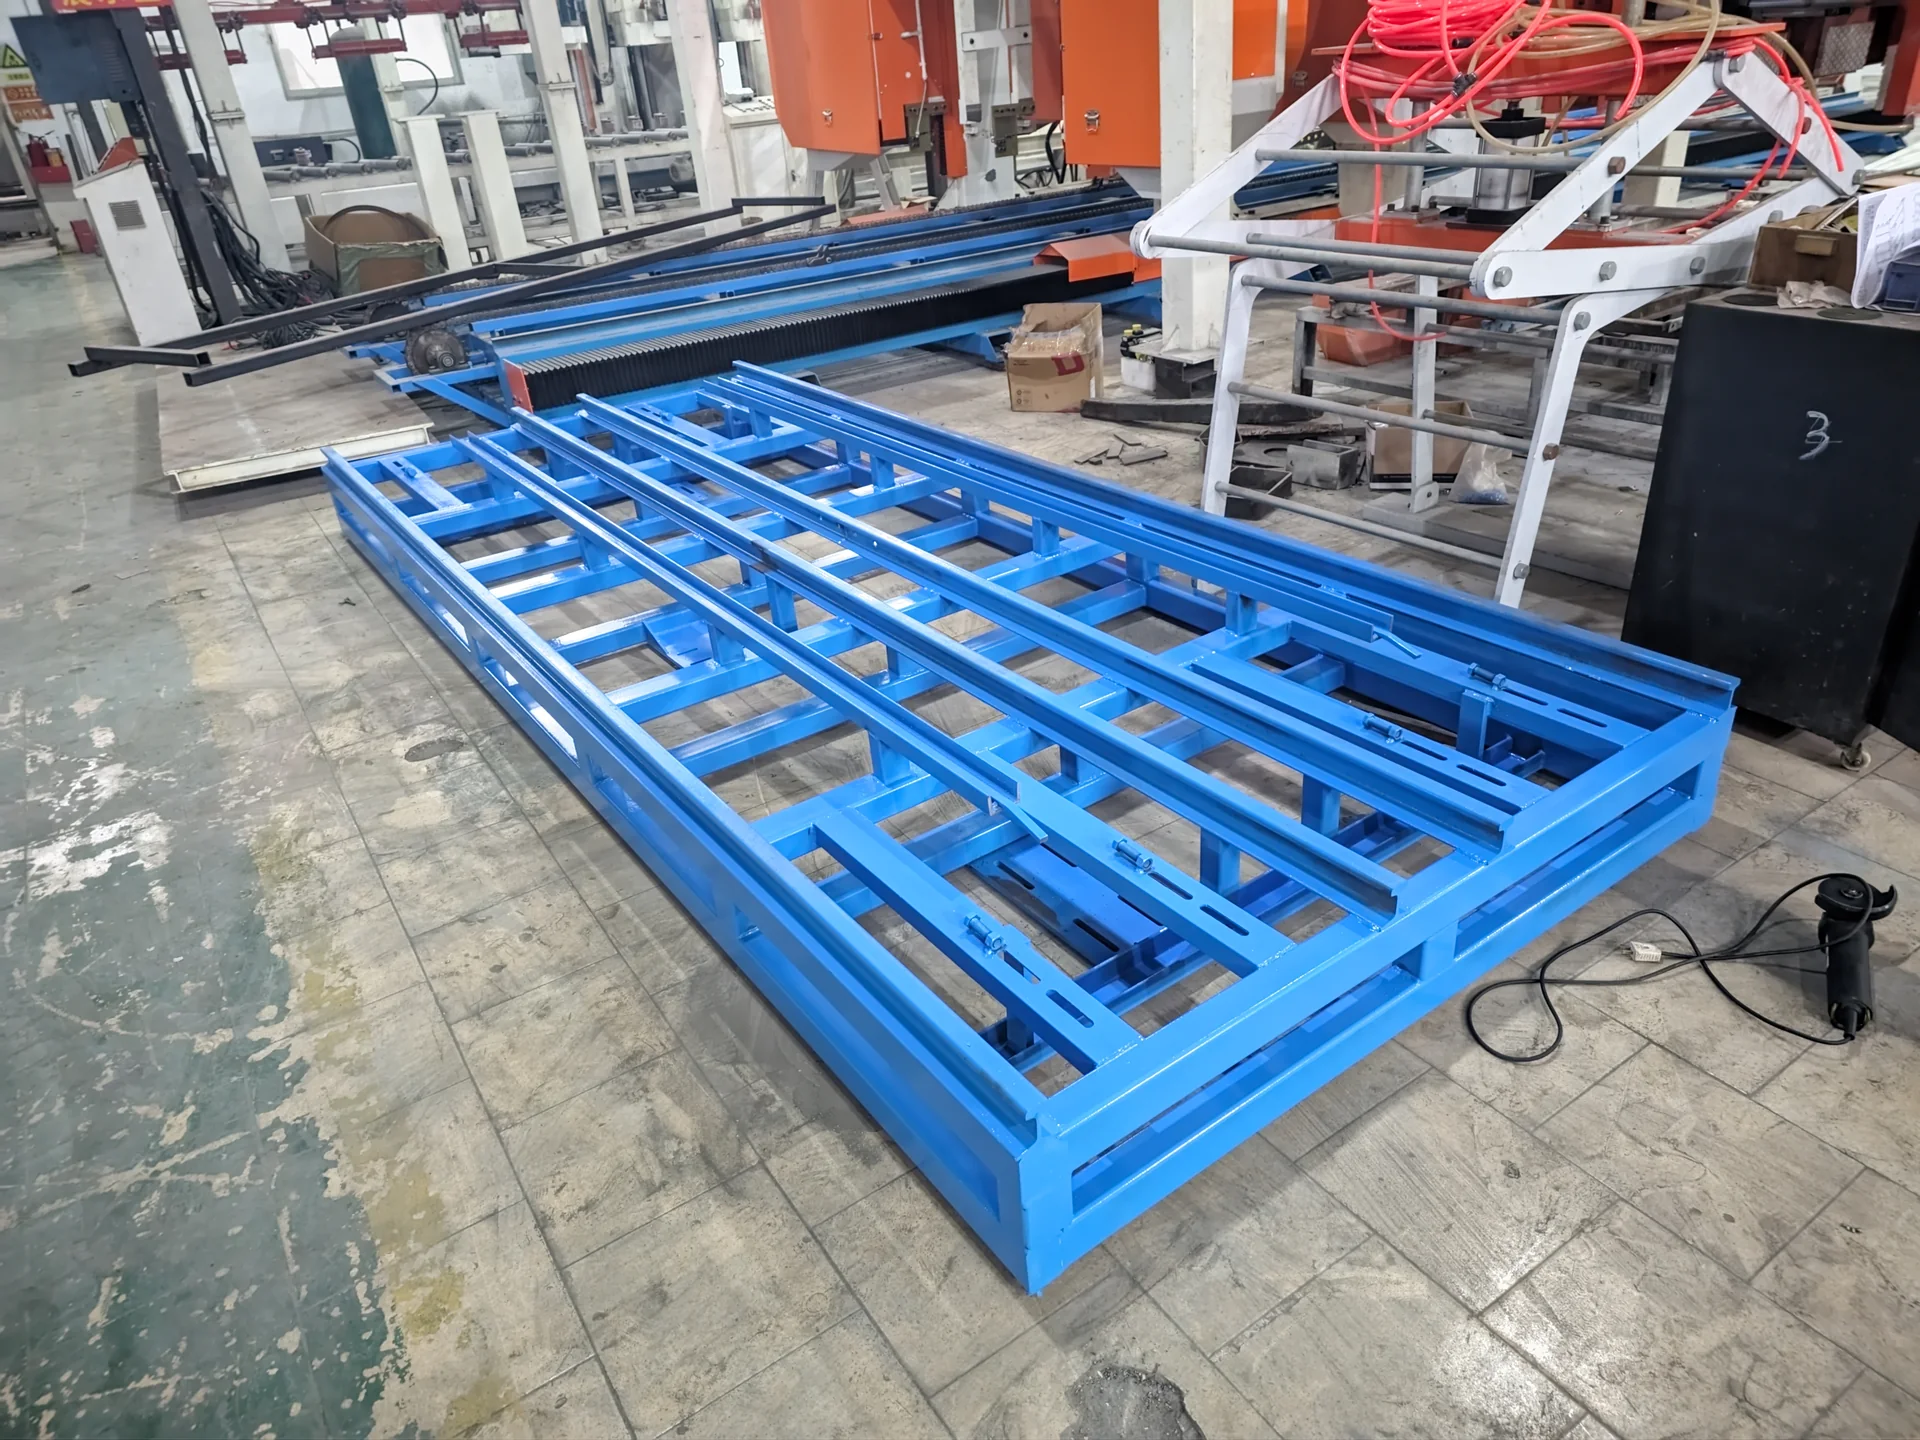
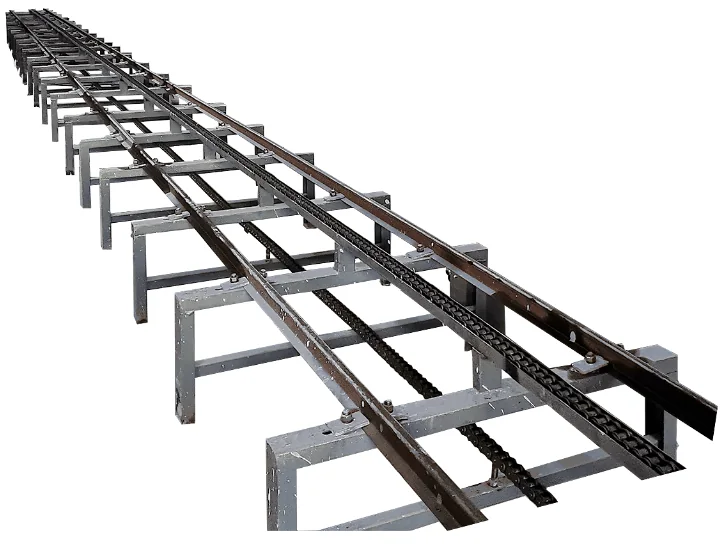
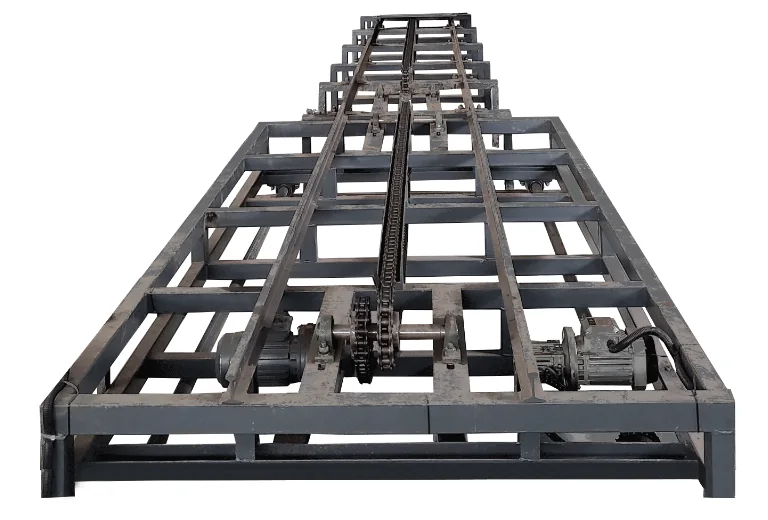
Drag or swipe through real equipment photos and engineering layouts. Open the main image to inspect it at full size.
PROJECT DELIVERY / TURNKEY SUPPORT
A factory proposal connects the project country, raw materials, target product and capacity, product dimensions, factory land, utilities, budget and automation requirement. The service and supply responsibilities are agreed for each project.
Evaluate representative samples from the project location before selecting the final process.
Adjust the formulation and material ratios against the test results and target product.
Confirm product dimensions and the product-specific preparation, forming, curing and finishing process.
Coordinate land, buildings, storage, material flow, foundations and utilities.
Match capacity, automation, budget, moulds and process interfaces to the agreed factory scope.
Prepare the agreed machines, tooling and controls against the approved configuration.
Check applicable equipment and delivery scope before shipment.
Coordinate packing, loading and destination requirements with the project shipping plan.
Install and connect the agreed equipment after site conditions are ready.
Check machine sequences and trial production with the selected materials.
Train operators in safe use, production sequence and routine maintenance.
Plan maintenance communication and spare-parts support for the installed equipment.
REAL HENGDE PROJECTS
HENGDE projects selected by product family, process route, capacity and current delivery stage.
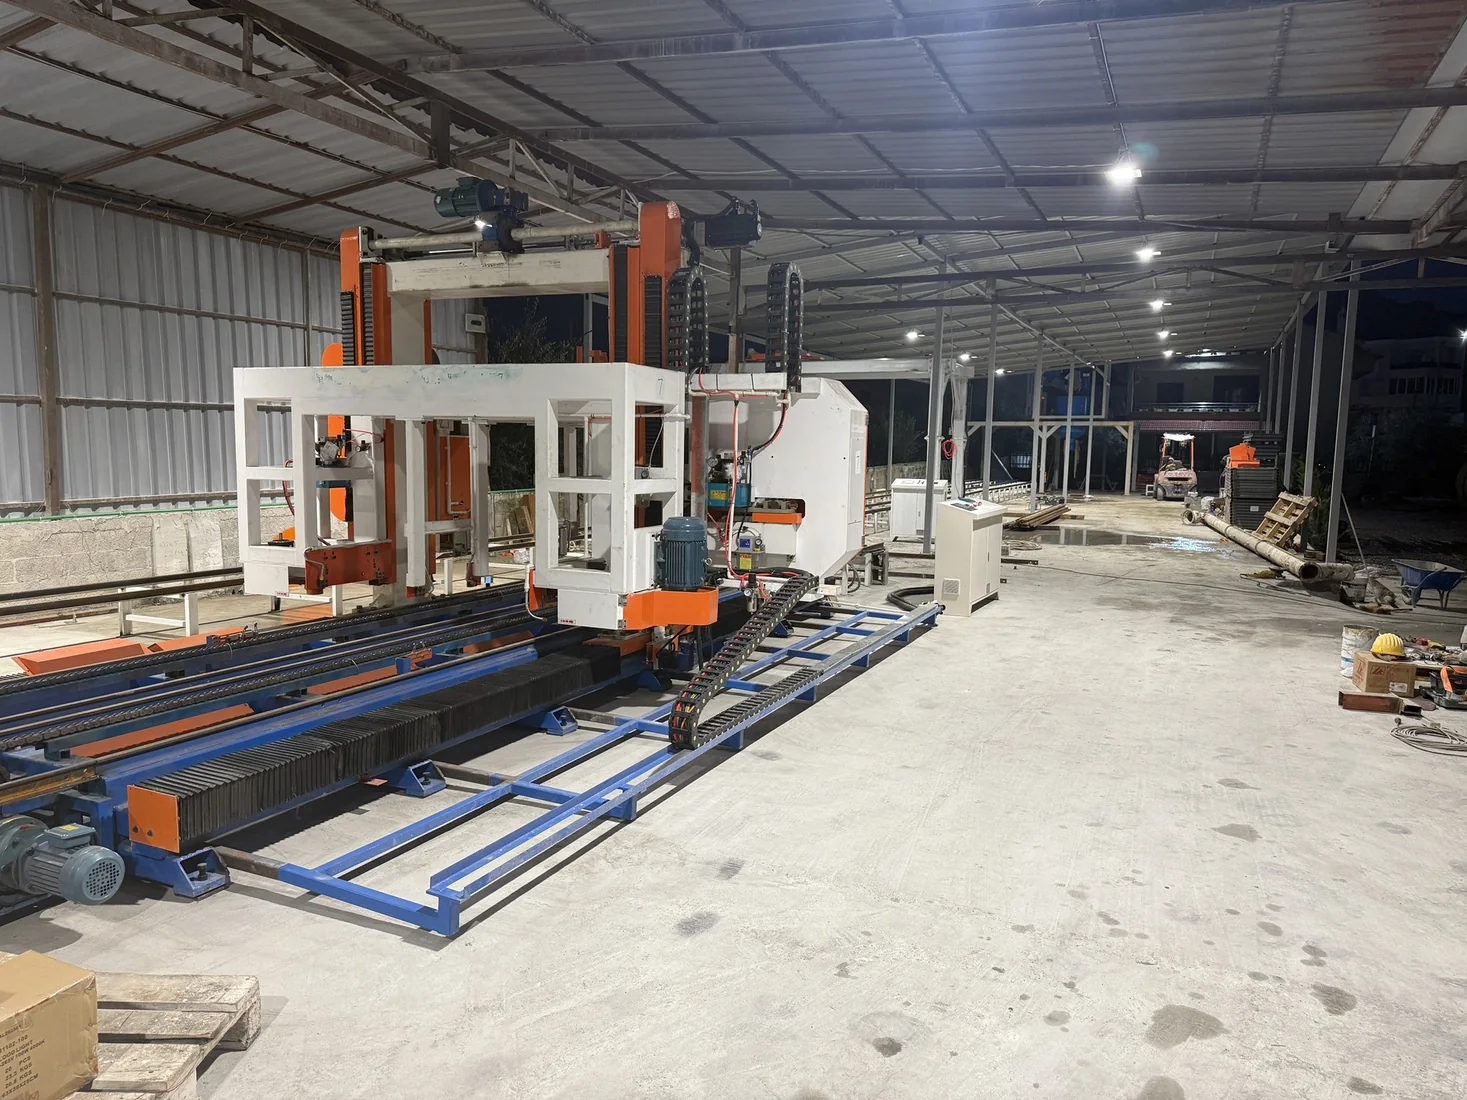 Tirana, Albania
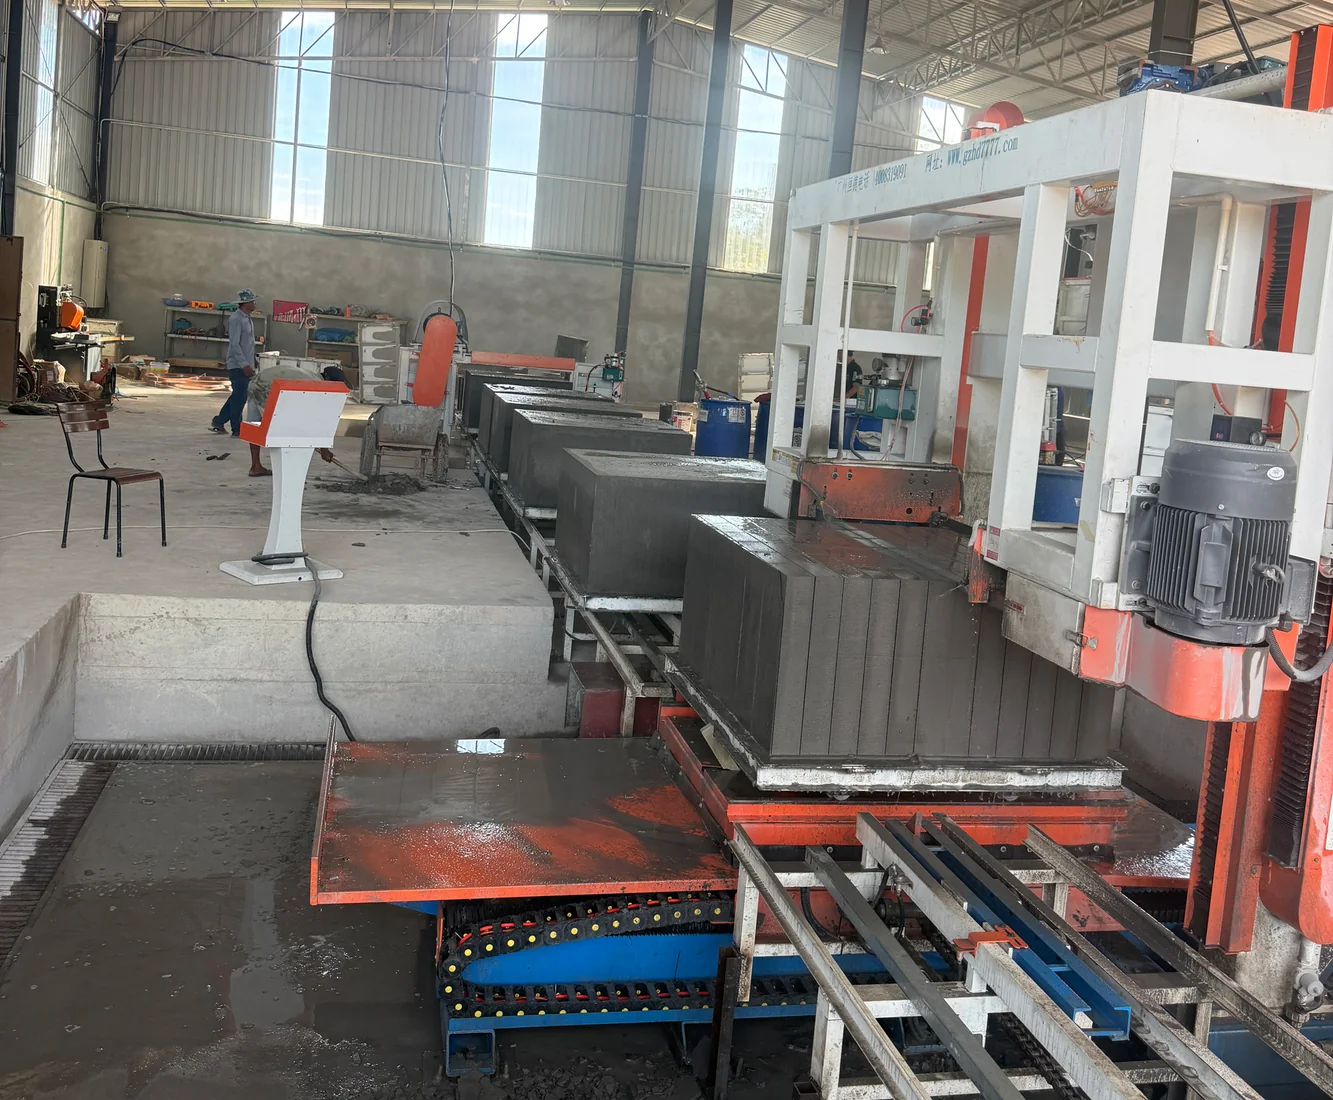 Phnom Penh, Cambodia
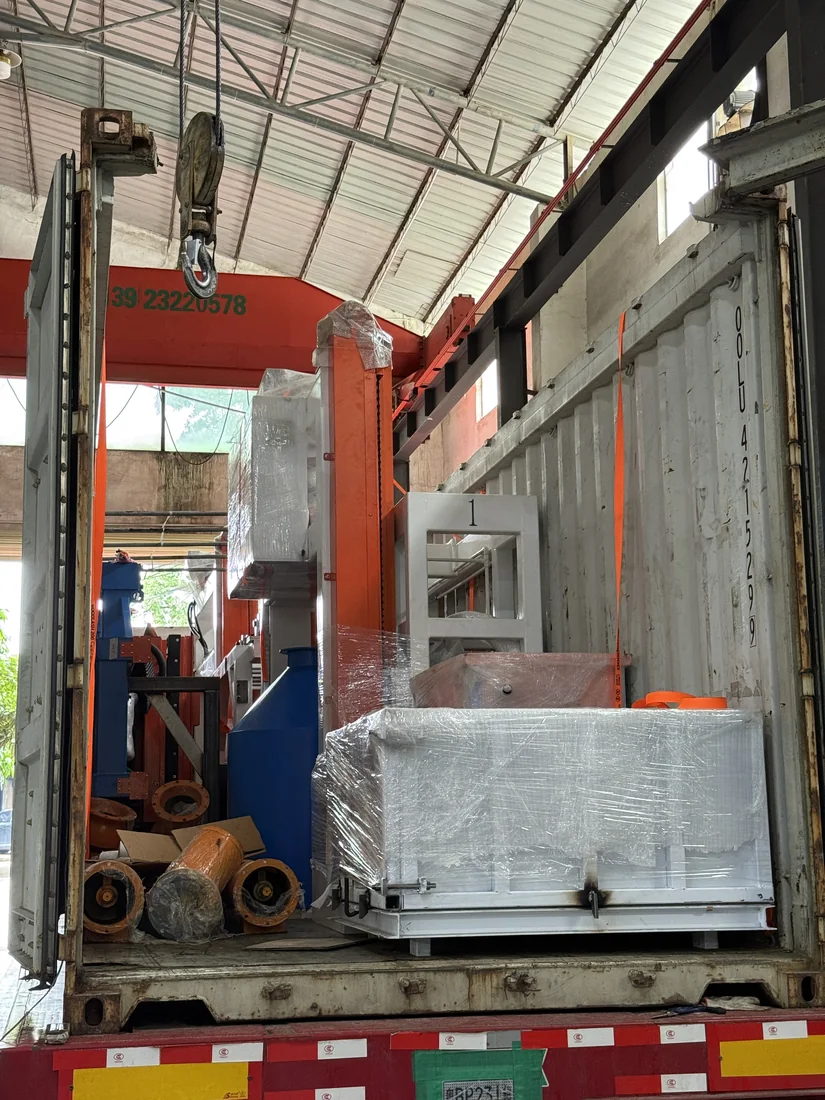 Indonesia
Review local binders, mineral inputs, process water and the physical-foaming system against this capacity-specific CLC configuration.
Review the available binder, mineral input, process water and physical-foaming input against the target CLC block.
Recycled mineral inputs require source-specific sorting, sampling and trial production before they enter the line design.
Test results guide slurry proportions, water ratio, preformed-foam dosage, mixing sequence and mould filling.
The confirmed curing, demoulding and cutting condition then determines mould circulation and downstream handling.
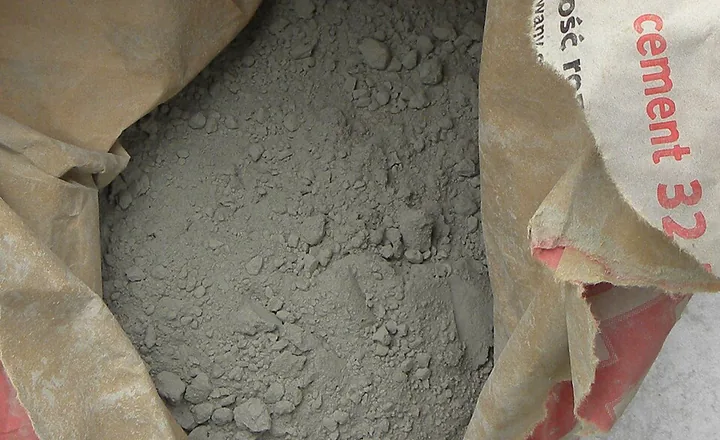
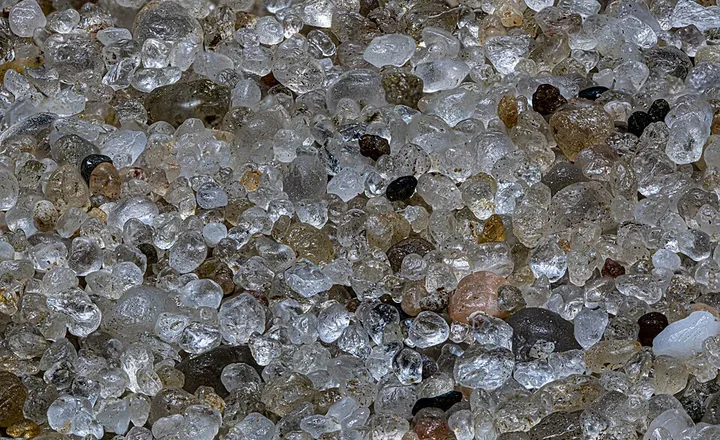
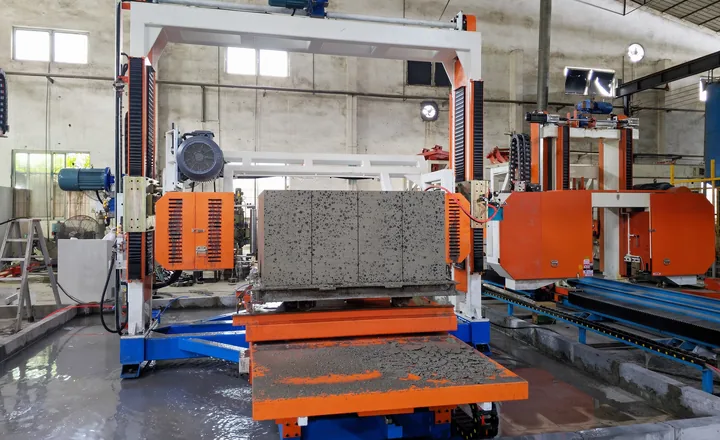
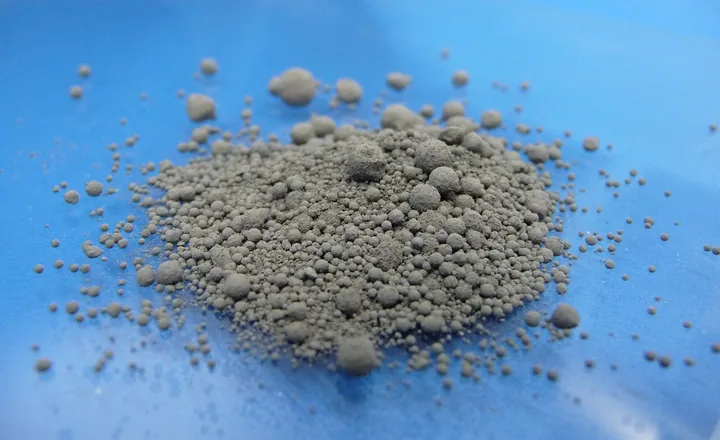
Sampling and project-specific review required.
Sampling and project-specific review required.
Sampling and project-specific review required.
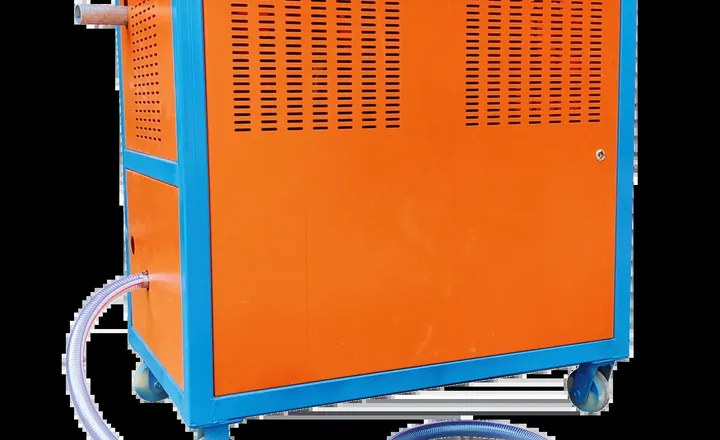
Sampling and project-specific review required.
A planned collection and settling loop can reduce uncontrolled slurry discharge and recover process water. The exact civil works, pump selection and reuse rate depend on the project layout and tested material system.
Raw-material availability varies by country. Send HENGDE your local material information before the final production-line configuration is confirmed.
Representative material photographs: cement, Szlomo Lejb / Sumek101; river sand, Krzem Anonim; fly ash, Ablazejo. Licensed under applicable CC BY-SA / GFDL terms. HENGDE project and testing photographs are identified separately.
PROJECT PLANNING
Tell us your target product, project location and planned output. The selected 200 m³/day configuration is included automatically.